

The Direct Buyer Answer
A CNC drilling and tapping machine is ready for production only when every critical hole and thread can pass a defined release gate across a realistic shift. Zhihe CNC starts with a controlled hole chart rather than maximum spindle speed. Record diameter, depth, position, tolerance, thread, chamfer, material, stock, fixture, tool, coolant, gauge and the feature that releases the part. This keeps speed connected to accepted output.
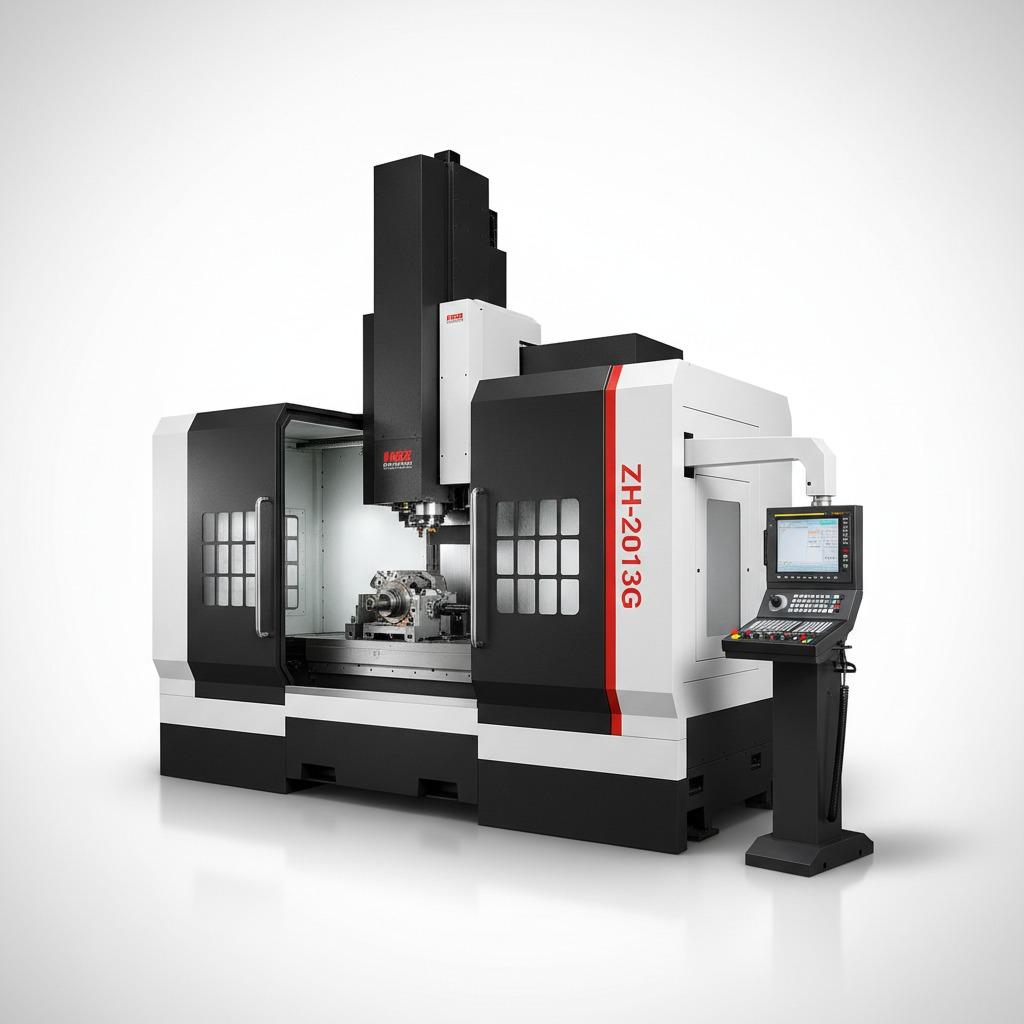
The Seven-Gate Board
| Gate | Release evidence | Stop signal |
|---|---|---|
| 1. Part identity | Drawing, material, stock and lot | Wrong or uncontrolled input |
| 2. Setup | Fixture, datum, tools, offsets and program | Unapproved setup state |
| 3. Hole | Size, position, depth and burr result | Feature outside limit |
| 4. Thread | Pitch, depth, entry and gauge result | Failed or uncertain thread |
| 5. Tool life | Trigger, replacement and verification | No controlled restart |
| 6. Takt | Complete time and released quantity | Spindle-only capacity claim |
| 7. Handoff | Backups, holds, open issues and owner | Next shift lacks status |
Gate 1: Freeze the Hole Chart
Group holes by diameter, depth, tolerance, orientation, thread and inspection. Mark blind, deep, intersecting or burr-sensitive features. A CNC drilling and tapping machine should be reviewed against the complete family because the easiest hole rarely controls the release decision. Zhihe CNC keeps the chart with the drawing revision so later changes are visible.
Gate 2: Record the Setup State
Capture fixture drawing, datum cleaning, clamp sequence, tool assemblies, holder projection, presets, program checksum, offsets, coolant and machine warm-up. Trial an unload and reload. If the result changes, separate seating, support, tool and measurement effects before editing multiple variables. The approved setup becomes a reproducible starting point rather than operator memory.
Gate 3: Release the Drilled Feature
For drilling, record size, position, depth, straightness when relevant, chamfer, burr and surface observation. Keep gauge identity, calibration status, sampling and raw data. A pass label without the measurement route is weak evidence. Zhihe CNC recommends preserving accepted and held pieces around the first tool-life event.
Gate 4: Release the Thread Separately
Thread quality needs its own evidence: tap type, pitch, depth, entry, reversal, lubrication, chip state, gauge and held-piece disposition. A good drilled hole does not prove the tapping route. For a CNC drilling and tapping machine, separate release gates make it clear whether a problem belongs to drilling, tapping, fixture, tool or inspection.
Hole and Thread Evidence Matrix
| Lane | Record | Reopen when |
|---|---|---|
| Geometry | Feature, datum, raw result and gauge | Drawing or gauge changes |
| Tooling | Tool, holder, preset, runout and life trigger | Tool or holder changes |
| Process | Feed, speed, coolant, chip state and program | Material or program changes |
| Release | Accepted, held, reworked and scrapped quantity | Sampling or decision changes |
Gate 5: Make Tool Life Auditable
Choose a controlled unit such as holes, parts or cutting time. Record tool batch, load, holder, preset, runout, wear, replacement trigger, affected features and restart verification. Include one planned replacement in the trial. A prepared cycle with fresh tools does not prove routine recovery or stable production.
Gate 6: Calculate Accepted Takt
Accepted takt equals declared production time divided by released parts. Include loading, cleaning, probing, drilling, tapping, tool changes, chip work, inspection, maintenance, held parts, rework and restart. Exclude time only when the commercial capacity model also excludes it. Zhihe CNC uses this ledger to distinguish fast cutting from supportable shift output.
Gate 7: Close the Shift
Transfer the hole chart, fixture state, tool library, presets, program, offsets, gauge status, accepted count, held work, maintenance, backups and escalation contacts. Name the next-shift owner. An unresolved hold must remain visible until an authorized release. This prevents a clean dashboard from hiding uncertain parts or missing tools.
Follow One Lot Through the Gates
Select a representative lot and connect material identity, setup, tool events, inspection, accepted quantity, holds and corrections. Compare early, middle and late pieces around a planned replacement. This does not establish a universal wear curve; it shows whether the declared control route protects the lot under tested conditions.
Stage a Safe Interruption
Use a programmed stop, tool-life trigger or inspection hold. Do not create unsafe conditions. Record machine state, affected quantity, containment, correction, retest and restart owner. A CNC drilling and tapping machine is commercially useful when the operating team can recover traceably, not only when the ideal sequence runs quickly.
Balance the Queue Around the Spindle
Map material, fixtures, presets, gauges, decisions and downstream transfer. Record waiting separately from working time. At higher output, small delays in gauge access, tool replenishment or held-work review can control released capacity. Zhihe CNC makes these queues visible before the buyer approves labor or automation assumptions.
Carry the Gates Into the Purchase Order
Attach the configuration, hole-family trial, gauge plan, tool-life method, accepted-takt definition, training, spare tools, service route and exclusions. Tie payment milestones to evidence instead of calendar dates alone. Product certification, fatigue, pressure performance and downstream assembly remain separate unless specifically contracted and tested.
Buyer FAQ: CNC Drilling and Tapping Machine
What should a hole chart contain?
Include geometry, material, orientation, tolerance, thread, tool, coolant, gauge and release rule.
Why separate drilling and tapping gates?
A correct hole does not automatically prove thread depth, entry, gauge result, chips or lubrication.
Is spindle speed a capacity measure?
No. Use released output after setup, tooling, chips, inspection, holds, maintenance and recovery.
Why include a planned tool replacement?
It shows whether preset, offsets and verification restore the approved route during a normal event.
What belongs in a held-part record?
Record identity, quantity, machine state, tool, result, containment, correction, retest, owner and decision.
How should chip control be reviewed?
Tie chip observations to material, depth, orientation, tool geometry, coolant and cleaning intervals.
What should shift handoff include?
Include configuration, tools, gauges, accepted count, held work, maintenance, backups and escalation.
How does Zhihe CNC review takt?
Zhihe CNC counts all declared production and support time against released parts.
When should evidence be reopened?
Reopen affected gates after drawing, material, fixture, tool, program, coolant, gauge, site or maintenance changes.
What should buyers request next?
Request a representative hole-family trial, raw gauge data, tool-life event and complete shift ledger.
Create a Release Passport for Every Trial Lot
A release passport should connect material identity, drawing revision, hole chart, fixture, program checksum, tool batches, presets, machine state, coolant, gauge identity, sampling and disposition. Give each pallet, tray or lot a visible identity. When a feature is held, the passport should show which parts may be affected and which evidence is needed before release. This prevents the inspection result from becoming detached from the setup that produced it.
Use the passport to compare parts before and after a planned tool replacement or shift handoff. Record the same release features, gauge route and correction history. For a CNC drilling and tapping machine, this comparison demonstrates whether routine events are controlled without pretending that one lot predicts every future material, tool or geometry. Preserve the original state and the approved corrected state.
Cost the Support Work Around Each Released Part
Build a practical cost ledger for fixtures, holders, drills, taps, coolant, gauges, presetting, tool replacement, inspection, chip handling, maintenance, held-work review and operator time. Do not invent a payback figure. Use the buyer's declared volume, part mix and working pattern so commercial teams can compare two routes with the same assumptions. A fast spindle cycle can still carry expensive manual or inspection work.
Review consumable and spare-tool ownership before the order. State supplied quantities, expected verification, reorder route, shelf or storage needs and the trigger that reopens the trial. Zhihe CNC recommends linking the ledger to accepted takt, because cost per released part is more useful than cost per ideal cycle. Keep unresolved assumptions, responsible people and review dates visible through commissioning.
Close the Final Approval Meeting
Before release, ask each function to state its open issue and the evidence needed to close it. Purchasing confirms scope and milestones; engineering confirms the hole family and configuration; quality confirms gauges and disposition; production confirms labor and takt; maintenance confirms care and spares; the supplier confirms service and exclusions. Record the decision, owner and date in one meeting file.
Label every unresolved item as a blocker, accepted limitation or post-release deliverable. An accepted limitation should name its operating consequence. A deliverable should have a due date and acceptance evidence. This final discipline keeps the technical trial connected to the commercial order and gives the receiving team a usable list instead of scattered messages.
Bring the Decision to Zhihe CNC
Send Zhihe CNC controlled drawings or CAD, material and stock, critical features, annual volume, batch mix, fixture ideas, tool constraints, inspection methods, site conditions and service region. Review the Zhihe CNC product portfolio, the company and factory profile, and the engineering inquiry route. For CNC drilling and tapping machine, ask for a dated configuration, representative trial, acceptance boundary, open-assumption list and named support owner.
Reference Boundary
The ISO 10791 machining-centre reference and the OSHA machine-guarding guidance provide machine-test or safeguarding context. They do not replace drawing-specific acceptance, local risk assessment, product certification, regulatory release or the buyer's operating procedures.





