

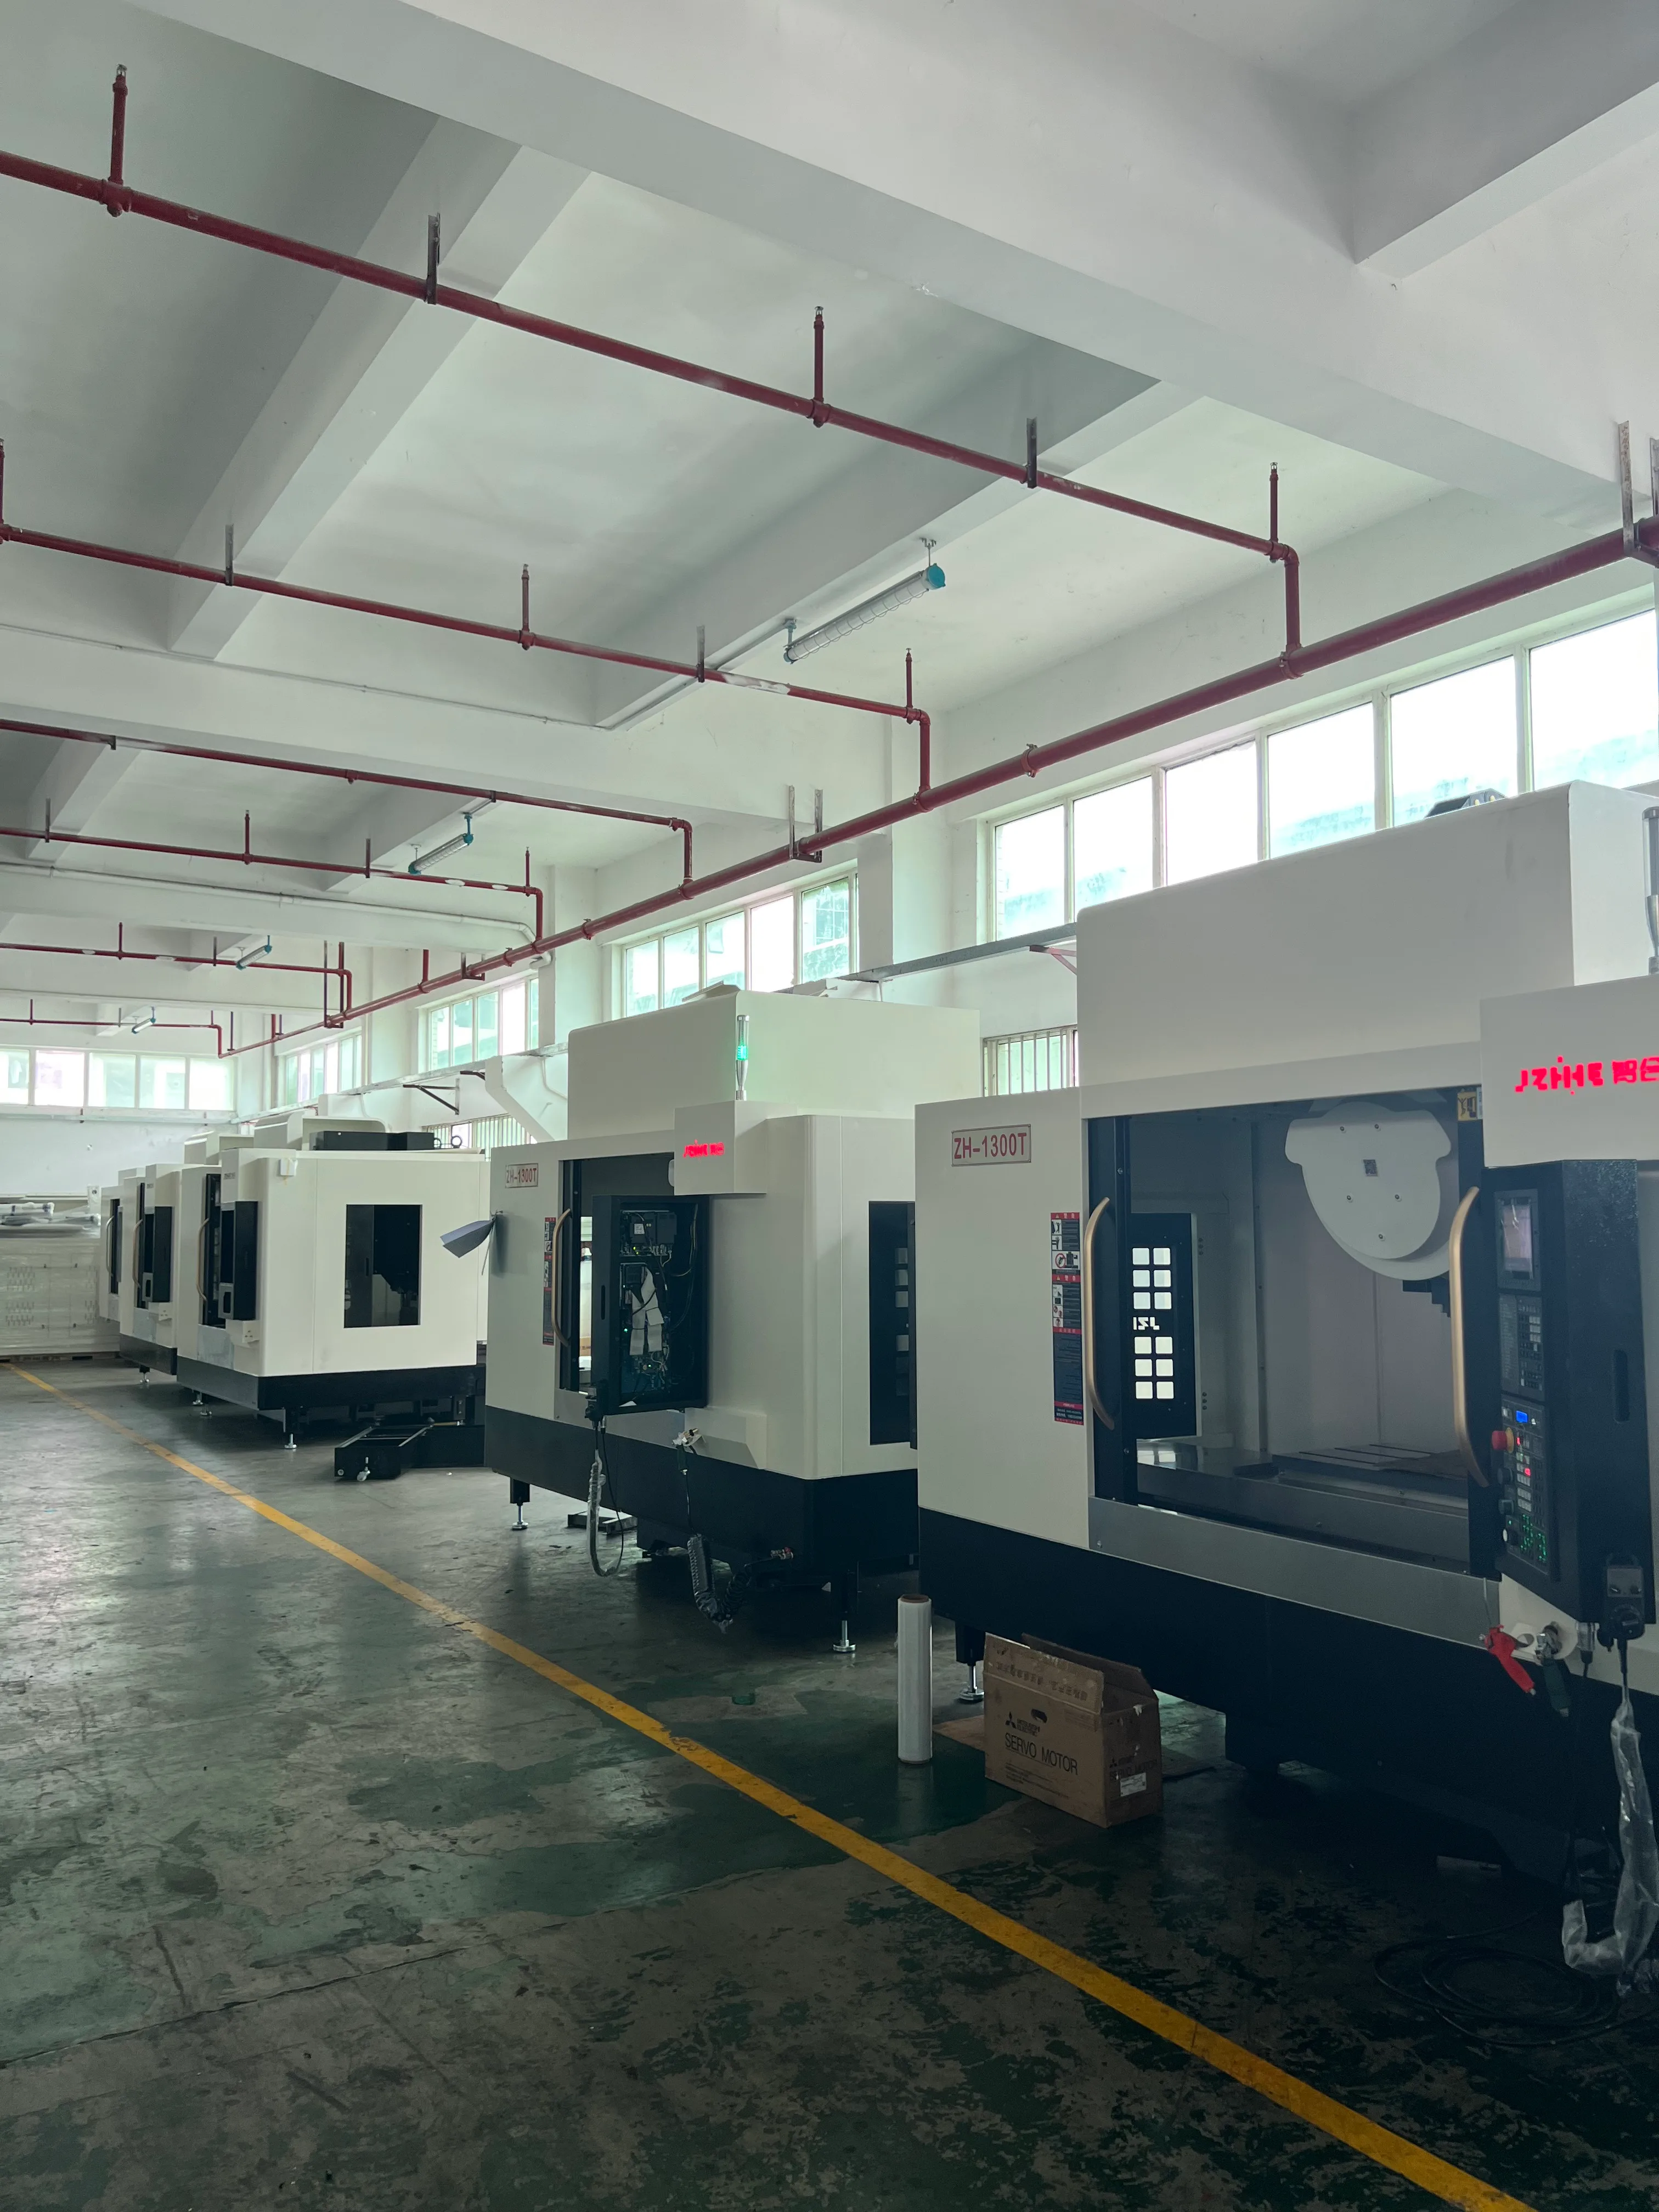
CNC machine compressed air requirements are often reduced to a single pressure number, but a pressure number cannot tell a plant whether enough clean air will arrive during a tool change with three machines starting together. A better deliverable is a state-by-state air balance: who uses air, when they use it, how much the distribution loses, what quality each function needs, and who owns the utility before and after the machine connection.
For a Zhihe CNC project, begin with the installation country, selected machine configuration, accessory list, measured supply conditions, intended production pattern, and the facility team responsible for the compressor room and piping. Zhihe CNC can provide configuration-specific machine-side information. The buyer's qualified team still owns the plant air system, local compliance, and the safe design of the utility connection.
Begin at the Air Handoff Point
Draw a line at the machine's documented air connection. On the facility side, record the compressor, dryer, filters, receiver, main header, branch piping, isolation valve, regulator, flexible connection, and any local drain. On the machine side, record the inlet requirements, internal treatment where supplied, valves, cylinders, seals, air-blast functions, and monitoring.
That line is more than a drawing convention. It identifies which pressure and quality data the factory must supply and which performance Zhihe CNC must document for the selected configuration. It also prevents a purchase order from implying that the machine includes plant-wide drying, storage, or piping when those items are actually buyer responsibilities.
Ask for a revision-controlled interface sheet. Every row should name a value, document, exclusion, or responsible person. "Normal shop air" is not an engineering boundary.
Turn Demand Into a State Table
Build the balance around operating states rather than a single maximum. Normal cutting, rapid positioning, simultaneous tool changes, door or pallet movement, cleaning, startup, standby, and a degraded-compressor event can create different demands. CNC machine compressed air requirements should show not only how much air each state needs, but which uses are simultaneous.
| Machine state | Air uses to identify | Facility question | Record to retain |
|---|---|---|---|
| Standby | Seals, purge, positioners, accessory holds | What remains energized or pressurized? | Configuration and isolation plan |
| Normal cycle | Tool changes, clamps, air blast, door motion | What is the representative cycle and duty? | Cycle assumptions and option list |
| Simultaneous event | Two or more functions calling at once | What pressure must remain at the inlet? | Approved balance and local design |
| Startup or recovery | Receiver recharge and valve movement | How does the header respond? | Facility test and owner |
| Service isolation | Stored pressure and trapped volume | What procedure safely removes energy? | Employer's energy-control record |
This table is a planning aid, not a pneumatic design. A qualified facility engineer should determine pipe size, compressor control, storage, treatment, and protective measures using the actual site and applicable requirements.
Separate Pressure From Stored Capacity
A compressor gauge can look stable while a branch pressure collapses for a few seconds. Dynamic pressure depends on compressor control, receiver volume, pipe size, fittings, filters, dryers, regulators, hose length, leakage, and the timing of each demand pulse.
Record pressure at meaningful points: compressor discharge, after treatment, main header, branch takeoff, and machine inlet during representative operations. Use instruments and methods accepted by the responsible team. A snapshot taken while the plant is idle is not evidence of peak performance.
The machine inlet may require a minimum pressure and a maximum pressure. Both matter. Too little pressure can prevent a clamp, tool change, or actuator from completing correctly. Excess pressure can increase leakage, wear, noise, and component stress. If the selected configuration has an allowable range, place it in the control document rather than relying on a verbal convention.
Specify Air Quality by Function
Air that is clean enough for a general cylinder may still be unsuitable for an air bearing, precision valve, blow-off near a sensitive surface, or measurement device. Conversely, treating every drop to the highest possible level can add unnecessary energy use and maintenance.
List each air consumer and the quality characteristics relevant to it. Depending on the application, that may include particulates, water, oil, pressure dew point, odor, or a customer-specific cleanliness requirement. The machine supplier should state what the selected equipment requires. The facility team should verify what its compressor room and distribution can deliver.
ISO 8573-1 is commonly used to classify compressed-air purity. The standard page can help teams identify the correct edition and scope, but it is not a substitute for the supplied machine documentation or a site-specific air-quality assessment.
Treat the Air System as a Chain
Compressed air does not improve accidentally as it travels. A dryer that is overloaded, a filter installed backwards, a blocked coalescer, a wet receiver, or a dead-leg branch can undermine an otherwise capable compressor room.
The U.S. Department of Energy's compressed air systems resource provides assessment material for industrial users. Use it as a starting point for the facility side of the balance, then apply the actual machine data and local requirements.
| Treatment or storage stage | Purpose to clarify | Evidence to request | Maintenance owner |
|---|---|---|---|
| Compressor and controls | Supply capacity and pressure control | Duty assumptions and service records | Facility |
| Aftercooler and dryer | Manage moisture and temperature | Treated-air data and load limits | Facility |
| Primary filtration | Protect headers and downstream equipment | Element specification and replacement rule | Facility |
| Receiver and drains | Buffer demand and remove liquid | Volume, control logic, and drain condition | Facility |
| Point-of-use treatment | Meet a specific machine or function need | Selected configuration and inlet requirement | Defined at handoff |
| Distribution and hose | Deliver dynamic flow with acceptable loss | Pressure survey and leak program | Facility |
The chain should be reviewed as a whole. If every stage is healthy but the branch is undersized, the machine inlet may still be unstable. If the header is strong but the point-of-use filter is neglected, contamination may reach the machine. Put a named owner and a measurable inspection interval against each stage.
Map Compressor and Receiver Behavior
A facility may have one fixed-speed compressor, a trim compressor, variable-speed units, a dedicated machine compressor, or several units under a central controller. Each arrangement responds differently when a large demand appears. Record which machine is lead, how the next unit starts, whether compressors load and unload frequently, and what happens during maintenance.
Receiver size is not automatically the answer to every pressure spike. Storage close to the demand can help, but the benefit depends on piping, control settings, check valves, and the time available to recharge. Ask the responsible engineer to model the actual event instead of adding a receiver by habit.
Also consider how compressed air is measured. A flow meter on the main header may not show individual branch loads. A machine feed meter may miss leakage and treatment losses. Define the boundary and the purpose of every measurement before comparing numbers.
Design Around the Failure State
The balance should identify what the machine does if pressure falls, quality degrades, or the compressor stops. Some functions may simply pause, while others may leave a part, door, or tool in a position that requires a controlled recovery. The machine's documented sequence and the employer's safety procedures govern.
Do not test a dangerous failure in production to discover the answer. Use the supplier's information, risk assessment, maintenance procedure, and approved commissioning plan. Confirm what is stored, what is monitored, what alarms are available, and who is authorized to restart the utility.
This is where CNC machine compressed air requirements become operational rather than commercial. The point is not to predict every outage. It is to make ownership and recovery steps visible before an outage happens.
Put the Air Balance Into the Project Record
The completed CNC machine compressed air requirements belong beside the quotation, approved drawing, and option list. When a dryer, filter, receiver, regulator, hose, or machine function changes, the balance should be revised and reviewed by the same responsible owners.
This record prevents a late accessory from being connected to an air source that was never assessed. It also gives service teams a starting point for troubleshooting without treating the original design as a permanent truth. CNC machine compressed air requirements are useful only while they describe the installed system.
Connect the Balance to Machine Functions
List the functions that rely on compressed air in the selected configuration: spindle or bearing purge, tool clamping, tool-change mechanisms, workholding, doors, pallet systems, cleaning nozzles, air gauging, and automation interfaces. Mark which are essential, which are intermittent, and which are optional.
For each function, record whether air is continuously supplied, pulsed, or held against a load. A small continuous purge and a large intermittent actuator create different facility tasks. If an accessory is buyer-supplied, keep it in the balance even when it is outside the machine scope.
The same discipline applies to future expansion. A machine purchased for a single part today may later run a pallet cell, robot, additional clamp, or automatic cleaning station. Record spare capacity assumptions as planning inputs, not guarantees.
Plan Monitoring and Alarms
Useful monitoring shows a condition before production quality or mechanical reliability is affected. Relevant signals may include inlet pressure, dew point, filter differential pressure, receiver condition, flow, or an alarm when pressure falls outside the accepted range. The exact instruments depend on the selected configuration and site risk.
Alarm text should identify the action: stop, hold, switch source, notify maintenance, or continue with a defined limitation. An alarm that only says "air fault" creates a slow response. A practical record explains who receives it, what they check first, and when production must stop.
Keep calibration and maintenance records with the instrument. A pressure switch that has drifted or a gauge that cannot be read in the installed position is not a reliable control.
Assign Maintenance and Ownership
Compressed-air maintenance crosses departments. Production may notice a pressure drop, maintenance may replace filters, facilities may control the compressor, and purchasing may own spare parts. The interface sheet should state who owns each asset and who can authorize a change.
Include filter replacement, drain inspection, leak repair, hose inspection, regulator checks, dryer service, receiver inspection, and instrument verification. Use the manufacturer's instructions and local requirements. Do not copy intervals from an unrelated machine.
When Zhihe CNC supplies a machine-side component, its maintenance information belongs in the delivered documentation. When the buyer supplies treatment, piping, or accessories, the facility team owns their condition. The boundary can change during a project, so update the sheet after every scope revision.
Review Installation and Commissioning
Before shipment, confirm the final air connection size, pressure range, quality requirement, flow assumptions, filtration, storage, isolation, drain, and monitor points. Recheck the CNC machine compressed air requirements against the selected options. Confirm that the machine location provides safe access for inspection and that hoses or piping will not be routed through traffic, heat, or contamination.
At commissioning, verify the connection and record the actual inlet condition under an approved test sequence. Check for leaks and unintended pressure loss. Confirm that alarms and interlocks behave as documented and that maintenance staff know how to isolate the supply. The facility owner should retain the final test record.
Do not use an ordinary production start as a substitute for commissioning. A trial can reveal real behavior, but it must have a defined purpose, boundary, acceptance criterion, and responsible observer.
Ten Buyer Questions About CNC Machine Compressed Air Requirements
What is the most important number to request?
Request the inlet pressure range and define the flow state or states in which it applies. A single pressure value without a demand condition is incomplete.
Should the pressure be measured at the compressor or the machine?
Measure at meaningful points on both sides of the handoff. Pressure loss through treatment, piping, filters, and hoses can change the condition at the machine inlet.
Who decides the required air quality?
The machine supplier states the selected equipment's requirement, while the buyer's qualified team verifies the facility can deliver and maintain it under applicable rules.
Is a larger receiver always better?
No. Storage helps only when it is correctly located and controlled for the demand event. The facility engineer should evaluate the system rather than add volume blindly.
Can one machine's air data be reused for another model?
Only as a preliminary reference. Tooling, actuators, purge, options, automation, and duty cycles can change the required flow and quality.
Should leakage be included in the balance?
Yes, as a facility loss that affects available supply. A leak-management program protects pressure, energy, and maintenance resources.
What happens if the compressor stops?
That depends on storage, control, machine functions, alarms, and the employer's procedures. Document the approved recovery path without inventing a universal rule.
Does dry air mean no maintenance is needed?
No. Dryers, filters, drains, regulators, hoses, receivers, and instruments still require inspection and service.
How should future options be handled?
List them as explicit planning cases with assumptions and owners. Do not promise spare capacity unless the responsible design has verified it.
What should the buyer send to Zhihe CNC?
Send the installation country, machine configuration, accessory list, facility air data, planned operating states, local review requirements, and the contact who owns the utility interface.
Close the Air Interface Before the Order Is Frozen
Review the Zhihe CNC machining-center portfolio and the company and manufacturing profile. Then use the engineering contact route to share the air balance, facility data, and final option list.
Ask for a dated configuration, machine-side inlet information, treatment and storage assumptions, monitoring points, documentation, and an open-issue register. Good CNC machine compressed air requirements do not promise that every plant is ready. They show where responsibility changes hands and what evidence must close each gap.





