

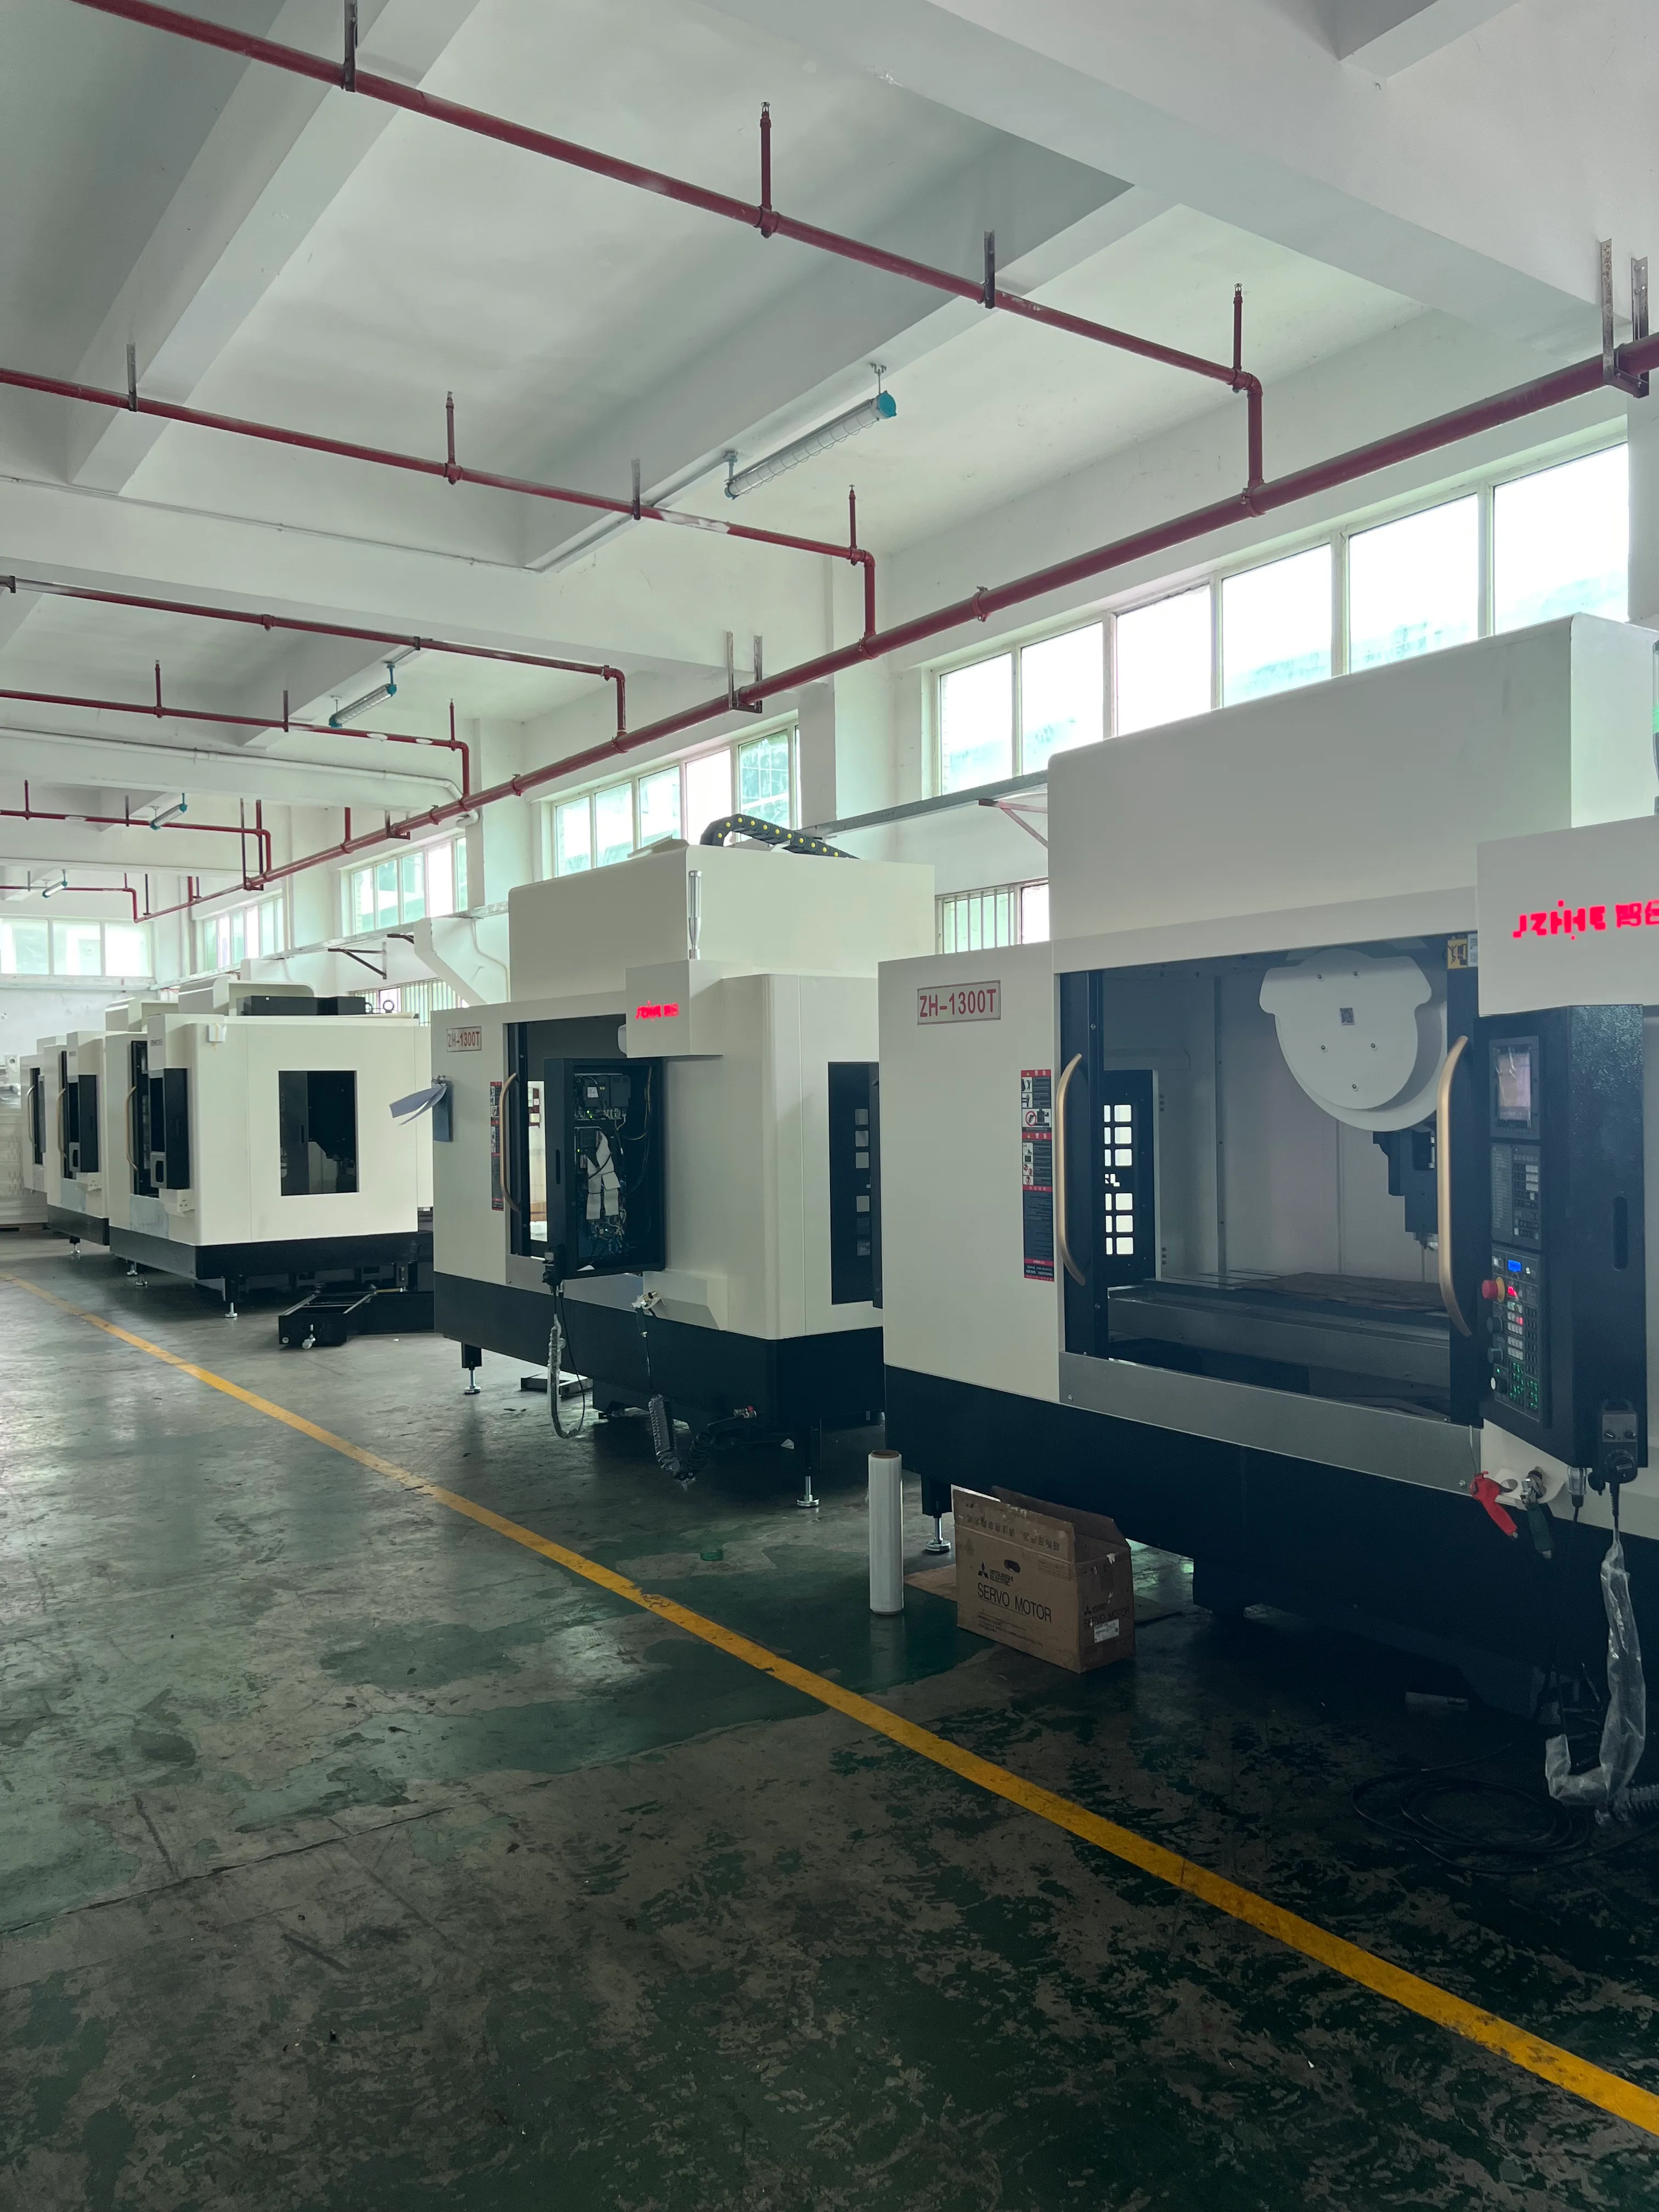
For machining center chip conveyor selection, the most useful RFQ attachment may be a container of representative chips. Drawings describe the finished part; chips reveal the material, cutting style, coolant carried out of the machine and the shapes that must travel through the removal system. A conveyor should be judged as part of the complete chip route, from the cutting zone to the factory's final collection point.
Zhihe CNC buyers can make this decision clearer by documenting chip form, generated volume, fines, long strings, mixed materials, shift pattern, unattended periods, cart access and coolant-return requirements. The supplier can then state which arrangement is proposed, what remains manual and what evidence will be shown during acceptance.
Begin With a Chip Sample Library
Collect samples from the common job and the boundary jobs. Label each sample with material, tool, operation, cutting condition, coolant state and approximate production interval. Do not rely on a specially tuned chip made for a showroom test. If the future process is not yet available, create a conservative description and mark it as an assumption.
Separate compact curls, needles, fines, nests and abrasive particles. Record whether chips are hot, sharp, oily, magnetic, buoyant or likely to bridge an opening. The names need not be perfect; photographs beside a scale and a physical sample are better than adjectives alone.
Sketch the Route Before Naming the Conveyor
The path begins where chips leave the tool. It includes table surfaces, telescopic covers, enclosure slopes, wash-down flow, troughs, augers, screens, the conveyor incline, discharge height and the receiving container. Any pocket along that route can become a manual cleaning task.
Walk the route with production and maintenance staff. Ask where operators currently use a hook, shovel, air gun or wash hose. Record safe isolation and guarding requirements for every intervention. A purchase decision should reduce uncontrolled contact, not simply move the difficult step out of sight.
Describe the Load in Time, Not Just Weight
Average kilograms per shift can hide short peaks. A roughing operation may release most of its chips during one part of the program. A pallet change may start the next cycle before the conveyor has cleared the previous load. The comparison should include peak generation, ordinary generation, idle intervals and the longest planned unattended period.
Use this test card to turn observations into comparable supplier responses.
| Test input | What to record | Why it changes the decision |
|---|---|---|
| Common chip | Shape, material, wetness and interval | Establishes routine transport behavior |
| Boundary chip | Longest, finest, sharpest or most abrasive sample | Exposes bridging, carryback or wear risk |
| Peak event | Program step and duration | Tests surge capacity instead of shift average |
| Mixed-material change | Cleanout target and separation need | Defines contamination and recycling responsibility |
| Unattended window | Maximum time without operator intervention | Sets expectations for alarms, cart volume and recovery |
| Coolant carryout | Wet chip condition and return path | Connects conveyor choice to coolant consumption |
This card makes machining center chip conveyor selection a production question rather than a catalog comparison.
Compare Mechanisms Without Declaring a Universal Winner
An auger, belt conveyor or filtered conveyor can be appropriate in the right application. Each name covers multiple designs, and option availability depends on the machine. Ask the supplier to explain the proposed mechanism against the supplied chips; this is the practical center of machining center chip conveyor selection.
Haas publishes separate official service information for a chip auger and a standard belt chip conveyor. Those pages are useful evidence that installation, belt condition, tension, motors and safety isolation create different service tasks. They are Haas procedures, not instructions or compatibility claims for a Zhihe machine.
| Arrangement to evaluate | Question it can answer | Risk to test | Maintenance evidence to request |
|---|---|---|---|
| Manual tray or basket | Is chip volume low and intervention acceptable? | Overflow, sharp-chip handling and forgotten cleaning | Removal method, capacity and safe access |
| Auger route | Can chips move through a compact trough? | Stringing, bridging, wear and drain blockage | Inspection points, reversal behavior and replacement access |
| Belt conveyor | Can continuous transport reach the cart? | Carryback, belt damage, tension and jams | Belt access, tension guidance and motor service route |
| Filtered conveyor | Must fines be removed from returning coolant? | Filter loading, bypass and consumable demand | Separation basis, monitoring and cleaning procedure |
| Multi-stage route | Are several collection zones involved? | Transfer between stages and hidden accumulation | Full flow diagram and synchronized control description |
Make Coolant Return Part of the Test
Wet chips carry valuable fluid out. Fine particles can pass back into the tank. A backed-up screen can make coolant pool inside the enclosure. Observe transport and return together. Record the state of the screen, tank and cart before and after a representative run.
Do not claim a recovery percentage without weighing or measuring under controlled conditions. Instead, define what will be observed: visible pooling, carryout, retained fines, filter loading and any manual wash-down. If a dryer, wringer or recycling station sits downstream, keep its performance and ownership separate from the machine conveyor.
Rehearse the Jam Before Production Depends on It
Create a safe, supplier-approved recovery drill. The purpose is not to deliberately damage equipment. It is to demonstrate how the system reports an abnormal condition, how energy is isolated, where accumulated chips can be accessed and who authorizes restart.
The drill should identify alarm text, stopped components, protected areas, tools, personal protection, lockout responsibilities, inspection after clearing and the condition for resuming automatic operation. Local safety rules and the delivered manual govern the actual procedure.
Put Guarding and Access in the Site Review
A moving conveyor introduces pinch, entanglement and sharp-material concerns. The interface with a cart or bin can also affect pedestrian routes and housekeeping. Review the installed arrangement, not only a component photograph. Include discharge height, cart changes, overflow containment, guarding, electrical connection and space for service.
The factory remains responsible for its risk assessment, training and work procedures. A supplier demonstration cannot certify every site condition. Record any guard, interlock or access change made after installation so that the original review does not become misleading.
Count Cart Changes and Cleaning as Production Work
Spindle-on time is not the only cost. Track conveyor run time, operator checks, cart changes, coolant drain time, cleanout between materials, planned inspection and recovery from stops. Use the buyer's real schedule and labor rates rather than a generic promise of "automatic chip removal."
For an unattended shift, define who responds to a full cart, stalled conveyor, abnormal noise or coolant overflow. If nobody can respond, the acceptable storage and alarm strategy changes. Machining center chip conveyor selection must match the staffing model as closely as it matches the chips.
Use a Two-Part Acceptance Trial
Part one is transport. Run the common and boundary chip conditions for an agreed window. Record peak events, interventions, carryback, visible accumulation and final cart state. Part two is recovery. Inspect accessible routes, clean the system using the approved method and verify restart after a controlled hold.
Keep the trial scope honest. A short test does not prove long-term wear, seasonal coolant behavior or every future material. It does show whether the proposed route is observable and whether responsibilities are understood. Attach that boundary to the machining center chip conveyor selection approval.
Specify the Commercial Boundary
The quotation should name the conveyor type, orientation, discharge side, cart or bin, controls, alarms, coolant-return elements, guards, installation work, utilities, documentation, wear parts and exclusions. Ask whether later retrofit is possible, but do not assume it. Interfaces can change with machine generation and layout, so close machining center chip conveyor selection against the dated machine configuration.
Zhihe CNC's product range provides machine categories for an initial discussion. The actual conveyor must be confirmed with the selected machine and process. Request a dated configuration drawing and a service-parts list before approval.
Ten Questions to Ask With the Chip Sample on the Table
Can one conveyor handle aluminum and steel chips?
It may transport both, but cleanout, recycling, fines and fluid compatibility can change the decision. Define the material-change procedure and acceptable cross-contamination.
Are stringy chips always a conveyor problem?
No. Tool geometry, cutting conditions and chip breaking also influence form. Treat cutting strategy and removal hardware as connected but separately owned controls.
Is conveyor capacity a single number?
Capacity depends on chip shape, bulk density, wetness, incline, peak loading and receiving container. Ask for the conditions behind any stated value.
When is an auger enough?
An auger may suit a compact route and manageable chips. Use representative samples to test bridging, wear, drain behavior and intervention frequency.
When should fine-particle filtration enter the comparison?
When particles affect returning coolant, process stability or downstream equipment. Define the particle problem and loading before selecting a filter label.
How should an unattended operation be reviewed?
State the unattended window, chip generation, cart volume, alarm path and response owner. Test the conditions that can stop or overflow the system.
What belongs in a conveyor maintenance plan?
Include inspection points, cleaning, tension or drive checks where applicable, lubrication, guards, sensors, wear parts and safe isolation steps from the delivered manual.
Does a successful short trial prove wear life?
No. It proves behavior only under the recorded sample and duration. Long-term wear depends on material, abrasiveness, loading and maintenance.
Should the chip cart be included in the quotation?
Yes, either as supplied equipment or a defined buyer interface. Record volume, height, drainage, handling method and safe changeover space.
Which chip evidence should accompany the RFQ?
Send chip samples or scaled photos, materials, operations, peak program steps, shift plan, unattended time, coolant, recycling rules, layout and preferred discharge direction.
Ask for a Chip-Route Drawing, Not a Feature Bullet
Use the Zhihe CNC contact page to submit the samples and test card. Ask the response to trace chips from the cutting zone to the collection point, identify manual work and define the acceptance trial.
Good machining center chip conveyor selection is visible in the dirty details: what arrives, where it travels, how coolant returns, how a stop is recovered and who owns the work. That route drawing will remain useful when production changes long after the quotation is signed.





