

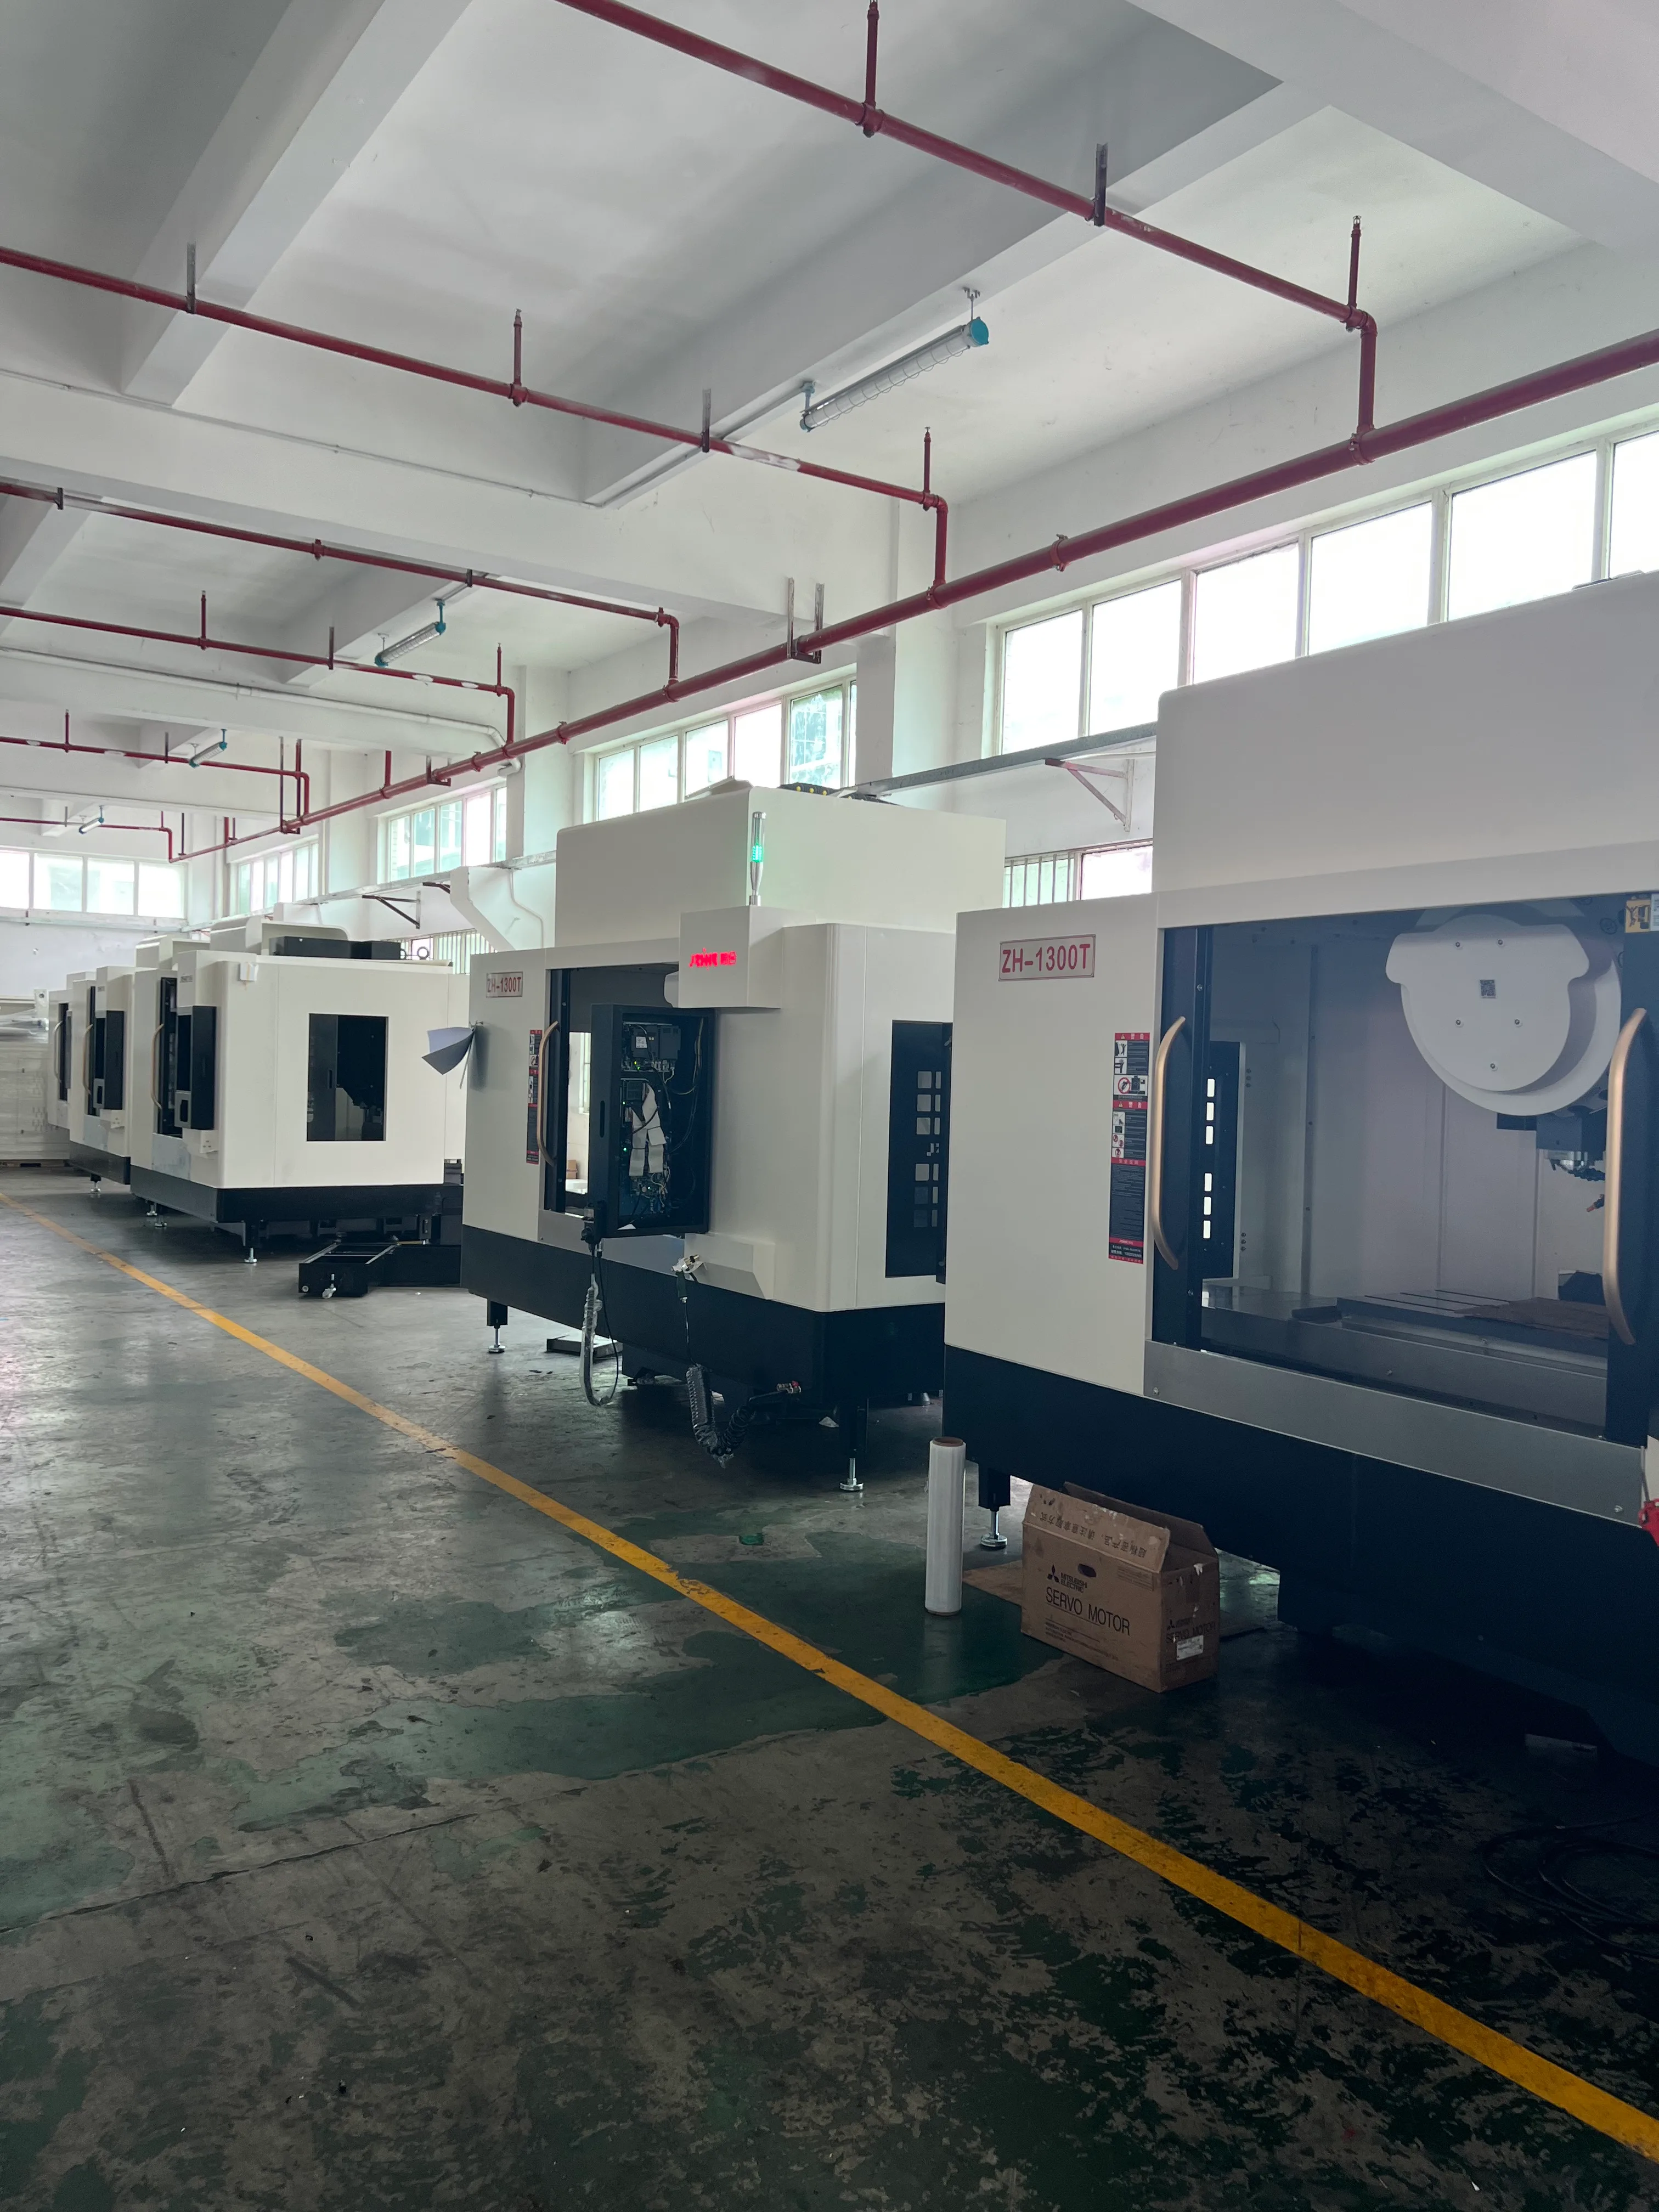
A useful CNC machine coolant system selection starts with the fluid after it has spent a week in production, not with the pump name printed on a quotation. The returning mixture carries evidence: fines, tramp oil, heat, air and whatever operators added during the shift. A system is suitable when it delivers fluid to the cut, brings it back without flooding the enclosure, separates what must be removed and gives the factory a manageable way to monitor the sump.
That makes coolant a production loop rather than an accessory. Buyers should define the workpiece, cutting process, fluid class, chip load, desired tool access, cleaning limits, worker-exposure controls and maintenance ownership before comparing options. Zhihe CNC can then review a proposed machine configuration against those declared conditions instead of assuming that one coolant package suits every part.
Follow One Liter Through the Entire Shift
Imagine marking one liter of mixed coolant as it leaves the tank. It passes the pump, hose and nozzle; reaches a rotating tool; collects heat and particles; falls through the enclosure; crosses a screen; and returns to the sump. Some of it becomes mist. Some remains on chips or parts. Some meets leaked lubricant. This is an illustrative tracing exercise, not a customer case or a promise about a specific machine.
Draw that path for the proposed operation. Mark every place where flow can be restricted, contamination can enter, fluid can be lost or an operator must intervene. The drawing immediately exposes questions that a pump-pressure figure cannot answer: Can the nozzle reach a deep pocket? Do fine chips bypass the screen? Is the tank accessible for cleaning? Where does overflow go? Who tests concentration after topping up?
Start With the Fluid Supplier's Operating Window
The fluid supplier should define mixture, compatible materials, water-quality assumptions, concentration range, monitoring method, storage, personal protection and disposal guidance. Obtain the current safety data sheet for the intended market. Do not copy a ratio from another workshop or treat a general online recommendation as the approved value for a purchased product.
OSHA's metalworking-fluid best-practices manual describes fluid selection, exposure control, enclosures, ventilation and fluid management as a connected system. Its guidance is useful for framing a buyer's questions. It does not replace the fluid supplier's instructions, local environmental rules or a site-specific safety assessment.
Build a Contamination Map Before Choosing Hardware
Record what enters the loop during ordinary work. The list may include alloy chips, abrasive fines, way lubricant, hydraulic oil, fixture debris, wash-down water and residue from part cleaning. Note whether different materials share the same machine and whether the fluid must remain compatible with seals, coatings and downstream processes.
The following table is an RFQ worksheet, not a specification for a Zhihe model.
| Stream point | Buyer evidence | Supplier response to request |
|---|---|---|
| Fresh mixture | Fluid product, water data, target range and SDS | Compatible tank, pump, seals and filling method |
| Cutting zone | Tool, feature, material and chip form | Delivery route, nozzle access and available pressure/flow data |
| Enclosure return | Expected chip volume, fines and wash-down practice | Drain, screen and return-path description |
| Sump | Shift pattern, idle periods and contamination sources | Tank access, monitoring points and cleaning method |
| Air and surfaces | Mist, splash and housekeeping concerns | Enclosure interfaces and optional extraction provisions |
| Waste route | Local handling and disposal plan | Drain points, retained volume and service precautions |
This map prevents an attractive option from solving the wrong problem. Through-tool delivery may help one deep feature yet add filtration and maintenance requirements. A larger tank may moderate temperature or extend service intervals in some processes, but it also contains more fluid to manage. The correct tradeoff depends on the documented loop, which is why CNC machine coolant system selection must start with process evidence.
Separate Delivery, Cooling, Lubrication and Chip Transport
Coolant can cool, lubricate, protect against corrosion and carry particles, but each process values those functions differently. A high-speed aluminum operation may emphasize heat removal and chip evacuation. A difficult tapping operation may demand reliable delivery at the tool. A mixed-material cell may make contamination control and cleanout the deciding factors.
Do not ask whether a system is simply "high pressure." Ask for the available operating range at the relevant interface, the conditions under which it is stated, and the filtration needed upstream. Long hoses, small passages, rotating unions, nozzles and loaded filters all belong in the discussion. Actual cutting performance still depends on the tool, material, program and workholding.
Treat the Sump as a Serviceable Work Area
Haas's official coolant-maintenance guidance emphasizes concentration control, suitable tools, tank cleaning and spill cleanup. It is written for Haas equipment, so it must not be presented as a Zhihe operating instruction. It does show why access and routine measurements deserve attention during equipment selection.
Ask someone from maintenance to act out the real work: sample the mixture, remove a screen, reach settled material, access the pump, drain the tank and clean a spill. Record the isolation steps and tools required. If a component can only be reached after moving another piece of equipment, that dependency belongs on the layout and in the maintenance estimate.
Compare Architectures by Consequence, Not by Feature Count
The table below organizes alternatives without claiming universal superiority or availability on every machine. Final options require configuration confirmation.
| Arrangement | Useful question | Added responsibility | Evidence for approval |
|---|---|---|---|
| Basic flood loop | Can stable flow reach every relevant cut? | Manual nozzle position and routine screen cleaning | Representative cutting and return-flow observation |
| Multiple directed nozzles | Do tools and fixtures block one another's flow? | Setup standard for nozzle positions | Recorded positions and worst-access feature trial |
| Through-tool delivery | Do internal passages need fluid at depth? | Tooling, filtration, sealing and interface compatibility | Approved tool path and pressure/flow condition |
| Additional filtration | Which particle size or contamination drives the need? | Filter monitoring, consumables and waste handling | Sample before/after the chosen separation step |
| Temperature management | Does measured drift justify added control? | Setpoint, heat rejection and service access | Temperature and part trend under a declared production window |
| Mist extraction interface | What exposure assessment and enclosure behavior apply? | Ducting, make-up air, filter service and local compliance | Site safety review and airflow verification |
The phrase CNC machine coolant system selection should therefore lead to a configuration sheet. It should not lead to a shopping list of every possible option.
Run a Dirty-System Trial, Not Only a Fresh-Tank Demo
A clean demonstration can confirm basic flow, but it says little about returning chips or a filter after production has begun. For a representative trial, define the material, stock, tools, duration, coolant product, initial concentration, water condition and chip load. Photograph or retain representative chips when practical. Log concentration and temperature at agreed intervals.
Observe nozzle stability, splash, pooling, drain behavior, visible fines, foaming, pump sound and operator interventions. After the run, inspect screens and accessible tank areas. If the trial is too short to represent contamination buildup, state that limitation rather than inventing a lifetime conclusion. Record that boundary in the CNC machine coolant system selection trial sheet.
Put Worker Exposure and Housekeeping Outside the Sales Claim
OSHA notes that poorly managed metalworking fluids can create skin and respiratory concerns, and its exposure-evaluation guidance discusses enclosures, splash control, fluid delivery and ventilation. The employer remains responsible for evaluating its workers, process and legal obligations. A machine enclosure or mist interface does not certify the finished workplace.
The purchase record should name who selects the fluid, reviews the SDS, evaluates mist, supplies extraction, trains employees, cleans spills and disposes of waste. Keep these duties visible in the quotation. Vague language such as "coolant system included" is not enough to close a safety or operating boundary.
Price the Loop for a Year of Use
Purchase price is only one line. Compare coolant volume, top-up practice, filters, skimmers, sensors, test equipment, cleaning labor, waste handling, planned stops and likely spares. Do not insert generic savings percentages. Use the buyer's labor rate, production calendar and fluid supplier's approved service assumptions.
For each optional component, ask what problem it addresses, what input it needs, what maintenance it adds and what happens when it is unavailable. This makes a CNC machine coolant system selection defensible even when two proposals use different architectures.
Write the Handover Around Measurements and Owners
The final package should include the purchased configuration, piping or flow diagram, approved fluids, filling and drain points, filter identities, consumables, maintenance instructions, alarm meanings and support contacts. Record baseline samples and any trial observations. Site procedures should add local safety, hygiene and disposal requirements. This document set is the lasting output of CNC machine coolant system selection.
Zhihe CNC's company profile describes machining-center manufacturing and project-based solutions. That context supports a configuration discussion; it does not establish the correct coolant package for an unnamed process. Send the real process envelope and request a dated response.
Ten Coolant Questions Buyers Usually Discover Late
Is a larger coolant tank always better?
No. Capacity must be considered with heat input, return flow, cleaning access, footprint and the volume the factory can maintain. Ask what operating problem the extra volume is intended to solve.
Can one fluid cover every material on the machine?
Only the fluid supplier and process review can answer that. Check material compatibility, mixed-metal contamination, tool requirements, corrosion protection and downstream cleaning before combining work.
What concentration should appear in the purchase specification?
Reference the selected fluid supplier's approved operating range and measurement method. Avoid setting a universal concentration without naming the product, water and process.
Does through-tool coolant eliminate external nozzles?
Not necessarily. Tool interfaces, drilling depth, face milling, washing and fixture geometry may create different needs. Review the complete tool list and flow path.
How should filtration be sized?
Start with the contaminant, particle range, generated load, required fluid cleanliness and service interval. Request performance under stated conditions rather than an unexplained filter label.
What should be measured during production?
At minimum, use the fluid supplier's requirements. Depending on the system, the plan may also track level, concentration, temperature, contamination, filter condition and corrective actions.
Who owns mist control?
The buyer should assign a site safety owner and define the supplier interface. Equipment features can support control, but workplace exposure and regulatory compliance require a site-specific evaluation.
Can coolant performance be accepted from one good part?
One part may confirm access and basic cutting. It cannot represent long-term contamination, microbial control, filter loading or every seasonal condition. State the evidence boundary.
What information should be included in a quotation?
List the tank, pumps, delivery paths, filtration, extraction interfaces, sensors, included consumables, utilities, maintenance access, exclusions and optional items by configuration.
What should I send Zhihe CNC first?
Send the material, fluid product or selection criteria, operations, tools, deepest features, expected chip load, shift pattern, finish concerns, site safety requirements and maintenance plan.
Turn the Coolant Loop Into an Engineering Inquiry
Before asking for a price, make a one-page fluid-path sketch and collect one representative chip sample. Mark the three points where the current process loses the most control. Then use the Zhihe CNC inquiry page to request a configuration review tied to those conditions.
A strong CNC machine coolant system selection ends with a measurable loop: approved input, controlled delivery, observable return, maintainable separation and named ownership. That record is more useful than an option list because it can be checked again when the material, tool or production schedule changes.





