

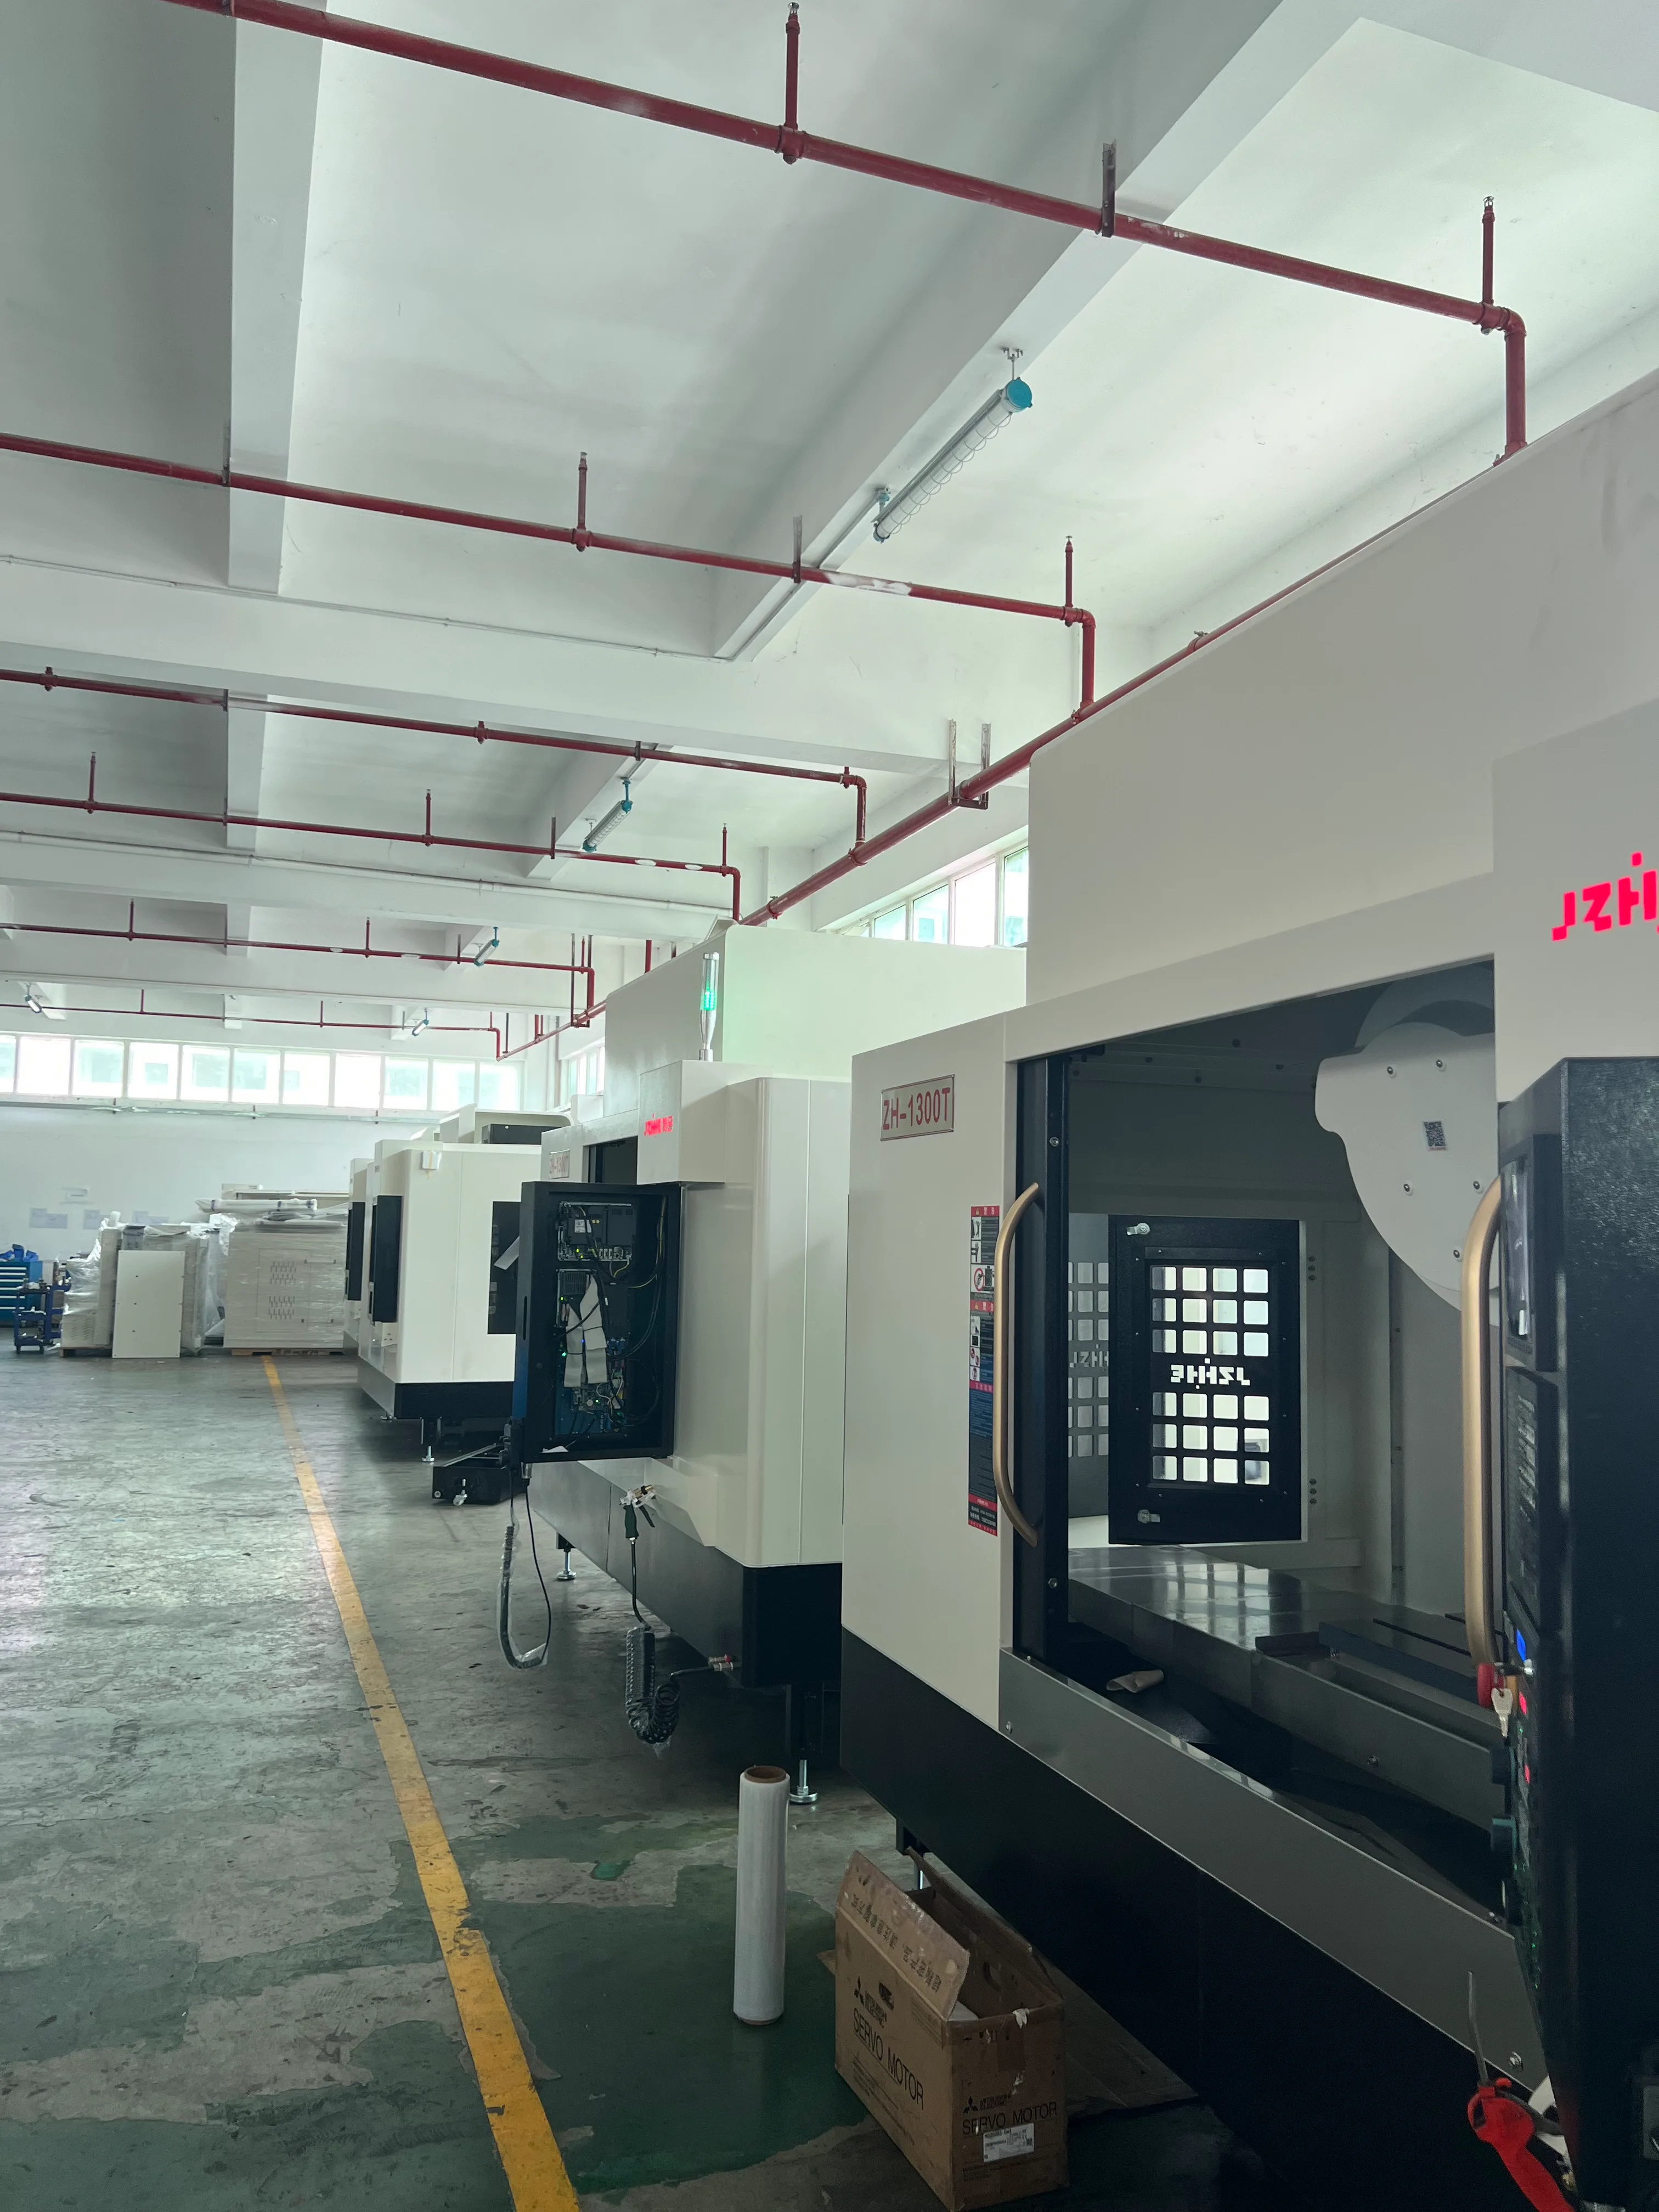
A CNC machine warm-up procedure should define what is being stabilized, how the factory observes it and when production may begin. Spindle rotation is only one part of the morning. Axes move, lubricant circulates, coolant changes temperature, fixtures settle and measurement equipment enters the same environment. The right procedure is the machine builder's approved routine joined to a part-specific release check.
For a Zhihe CNC project, the buyer should provide the shift pattern, idle periods, spindle range, tolerance-sensitive features, ambient conditions and inspection method. The supplier should return the approved startup steps for the selected configuration and identify conditions that require a different routine. A generic warm-up copied from another machine is not an acceptance document.
06:40 — Record the Cold Starting State
Imagine an early shift entering a workshop after a cool weekend. At 06:40, the operator records ambient temperature, machine display temperature where available, idle duration, coolant state and any active alarms. At 06:45, the approved machine checks begin. This is a sample timeline for planning, not an operating instruction or a claim about a Zhihe machine.
The record needs a stable reference. "Cold" is too vague. Note the time since last operation and any unusual condition such as a power outage, maintenance event, spindle replacement or large weather change. Those events may require instructions beyond the daily routine, so the escalation path belongs beside the checklist.
06:45 — Confirm Safety and Lubrication Before Motion
Follow the delivered manual and local safety procedure. Check guards, doors, work area, lubrication status, coolant level and the conditions required before automatic motion. The person performing the check must know which alarm or observation stops the sequence and who can authorize further action.
Warm-up should never be used to mask an unresolved noise, vibration, leak or lubrication problem. Record the symptom and hold production. The difference between "continue to stabilize" and "stop for diagnosis" needs to be explicit.
06:50 — Run the Approved Machine Sequence
Haas publishes a machine-specific spindle run-in and warm-up reference. It distinguishes installation run-in, ordinary warm-up and break-in after spindle work, with requirements tied to Haas configurations. That distinction is the useful lesson; its program numbers, durations and limits must not be transferred to a Zhihe machine.
Request the correct program or sequence for the purchased spindle, control and lubrication system. Record whether a toolholder is required, what speed stages apply, whether axes or coolant should operate and what conditions trigger an extended procedure. Keep revision control on the program just as you would on a production program.
07:05 — Watch Trends Instead of Hunting One Magic Temperature
Thermal behavior develops over time and may appear differently at the spindle, axes, coolant, fixture and part. One handheld reading cannot describe the whole machine. Choose a small set of observations that relate to the critical workpiece feature.
Renishaw's application note on heat and ballscrew accuracy demonstrates that heat buildup and feedback configuration can affect axis behavior. It is a specific study, not a universal correction value. It supports measuring a trend under declared conditions rather than assuming every machine moves by the same amount.
| Time point | Machine/process record | Part or reference check | Decision |
|---|---|---|---|
| Cold start | Idle time, ambient state and alarms | Identified artifact or first blank | Start only if preconditions pass |
| Sequence midpoint | Spindle stage, axes, coolant and observations | Optional reference trend | Continue, hold or escalate by approved rule |
| Sequence end | Completed program revision and exceptions | Reference feature before production | Release trial part or extend observation |
| First part | Tools, offsets, material and cycle state | Critical features in declared support state | Accept, correct with authority or hold |
| Later check | Elapsed production, ambient change and tool events | Same selected features | Confirm stability or reopen the plan |
The table makes the CNC machine warm-up procedure auditable without pretending that one schedule fits every tolerance.
07:10 — Choose a Reference That Answers the Production Question
A reference artifact can show a machine trend, but it does not automatically prove the process. A first part adds material, fixture, tools and inspection. For a high-mix factory, a simple reference may be more repeatable than machining a different production part every morning. The release plan can use both if each has a clear purpose.
Identify the datum, probing or measurement method, support condition and acceptable decision limit. Do not quietly adjust offsets until a reading looks good. Record corrections with the feature, amount, authority and reason so the team can distinguish thermal response from tool wear, material variation or measurement error.
07:20 — Release the First Part With Its Conditions Attached
The first accepted part should carry context: machine identity, program revision, tool status, fixture, material, warm-up record, inspection equipment and time. If the part is measured away from the machine, record the transfer and stabilization rule. A result without conditions is hard to compare the next morning or to improve the CNC machine warm-up procedure.
When a feature misses its limit, use a defined containment route. Check the measurement method, tool, offsets, support and recent maintenance before deciding that more warm-up is the answer. The purpose is to find the controlling variable, not to force every symptom into a temperature story.
09:00 — Recheck the Feature That Is Most Likely to Move
A later measurement helps show whether the release condition remains representative. Choose a feature connected to the risk: a bore location, length, height, flatness relationship or tool reference. The exact choice belongs to the process engineer and drawing.
Plot the value against elapsed time, ambient state and production events. Several mornings can reveal a pattern that one trial cannot. If the trend changes after maintenance, a new fixture, different coolant behavior or a seasonal shift, reopen the baseline rather than preserving an obsolete correction.
Compare Startup Policies by Lost Risk, Not Minutes
Three factories can buy similar machines and need different release policies. A job shop making tolerant parts may use the builder's routine plus a simple first-piece check. A tight-tolerance cell may need a reference trend and controlled measurement environment. An unattended cell may require automated checks and a hold path before people arrive.
| Production context | Practical release evidence | Hidden cost to count | Question for the proposal |
|---|---|---|---|
| One shift, common parts | Approved warm-up plus first-piece inspection | Operator time and delayed first cycle | What event restarts the sequence? |
| High-speed intermittent work | Builder-approved spindle sequence and tool condition | Idle gaps and balanced-tool requirements | Which spindle/configuration rules apply? |
| Tight feature relationships | Reference trend plus controlled part measurement | Gauging, environment and correction review | What data defines stable enough? |
| Mixed shifts | Shared log and role-based handover | Inconsistent starts and duplicated checks | Who owns release on each shift? |
| Unattended startup | Automated status, measurement and fault hold | Sensors, logic and response availability | How is an exception contained? |
This comparison does not assign a universal time or tolerance. It turns CNC machine warm-up procedure planning into a production-risk decision.
Make Idle Time and Restart Events Visible
Daily startup is not the only case. Lunch stops, weekends, planned shutdowns, loss of power, transport, spindle service and lubrication work can create different requirements. Build an event matrix from the delivered documentation. Each row should point to the approved sequence, required check and responsible role.
Do not let operators reconstruct instructions from memory. Store the controlled routine at the machine, protect the master version and record changes. Training should include the reason for each stop condition, not only the buttons to press. Revision control keeps the CNC machine warm-up procedure consistent across shifts.
Separate Warm-Up From Capability and Calibration
Completing a routine does not certify geometry, process capability or product conformance. Calibration evidence answers a defined measurement question. A capability study needs its own sample, conditions and analysis. First-piece inspection releases the stated work under the declared method.
Use different records for these purposes and link them by date and configuration. That boundary prevents a normal startup check from being quoted later as proof of every accuracy requirement.
Put the Routine Into Machine Selection and Acceptance
During purchase, ask how the spindle, axis feedback, coolant, enclosure, probing and optional temperature-related functions affect startup. Do not assume an option eliminates warm-up or guarantees an accuracy result. Request the configuration-specific manual, sequence and training scope, and name the CNC machine warm-up procedure revision in the acceptance record.
Acceptance can include a witnessed cold-start exercise if it matters to production. Agree the prior idle condition, reference, measurements, duration, operator actions and pass/fail decisions. A single demonstration should be labeled for what it proves and what it does not.
Ten Questions for the First Shift
How long should a CNC machine warm up?
Use the selected machine builder's current instructions and the process release evidence. A universal duration cannot account for spindle type, idle period, environment and tolerance.
Is spindle warm-up the same as machine warm-up?
No. Spindle rotation may be one element. Axes, lubrication, coolant, fixture, environment and measurement can affect the production release decision.
Can the first part be used as the reference?
Yes, when its material, fixture, tools and measurement are controlled. A separate artifact may provide a more repeatable machine trend for high-mix work.
Should offsets be changed during startup?
Only under an approved correction rule with traceability and authority. First verify measurement, tooling, fixture and recent events so a different cause is not hidden.
What happens after a weekend shutdown?
Follow the event-specific builder instructions. Record the idle duration and any environmental, power or maintenance changes that alter the normal routine.
Does probing replace first-piece inspection?
Not automatically. A probe measures defined features in the machine environment. Product release may require a separate method, support state or independent inspection.
Should coolant run during the sequence?
Use the approved configuration-specific procedure and process plan. Coolant circulation can affect temperature and readiness, but the correct method is not universal.
How should a warm-up exception be handled?
Stop at the defined gate, preserve readings and symptoms, contain affected work and send the record to the responsible technical or maintenance owner.
Can a stable morning prove all-day stability?
No. Add later checks at intervals connected to the process risk, ambient changes and production events. Review trends across several comparable days.
Which cold-start facts should reach Zhihe CNC?
Send shift times, idle periods, spindle use, critical features, tolerances, inspection method, ambient range, current startup losses and required acceptance evidence.
Close the Timeline With a Named Release Owner
Review the Zhihe CNC machining-center range, then submit the real startup conditions through the contact page. Ask for the approved sequence, required utilities and lubrication state, applicable options, training deliverables and cold-start acceptance boundary.
A durable CNC machine warm-up procedure tells the next operator what happened before the first part, why production was released and which event requires the evidence to be collected again. That is more valuable than a timer with no connection to the workpiece.





