

The Direct Buyer Answer
Fixture plates are interface parts: their value depends on flatness, hole relationships, datum stability, clamp access and the ability to reload work without guessing. A CNC machining center for fixture plates should therefore be selected through a datum contract. Zhihe CNC links the drawing, stock, support, drilling, tapping, probing, inspection and handoff so the plate becomes a reliable reference for later production.
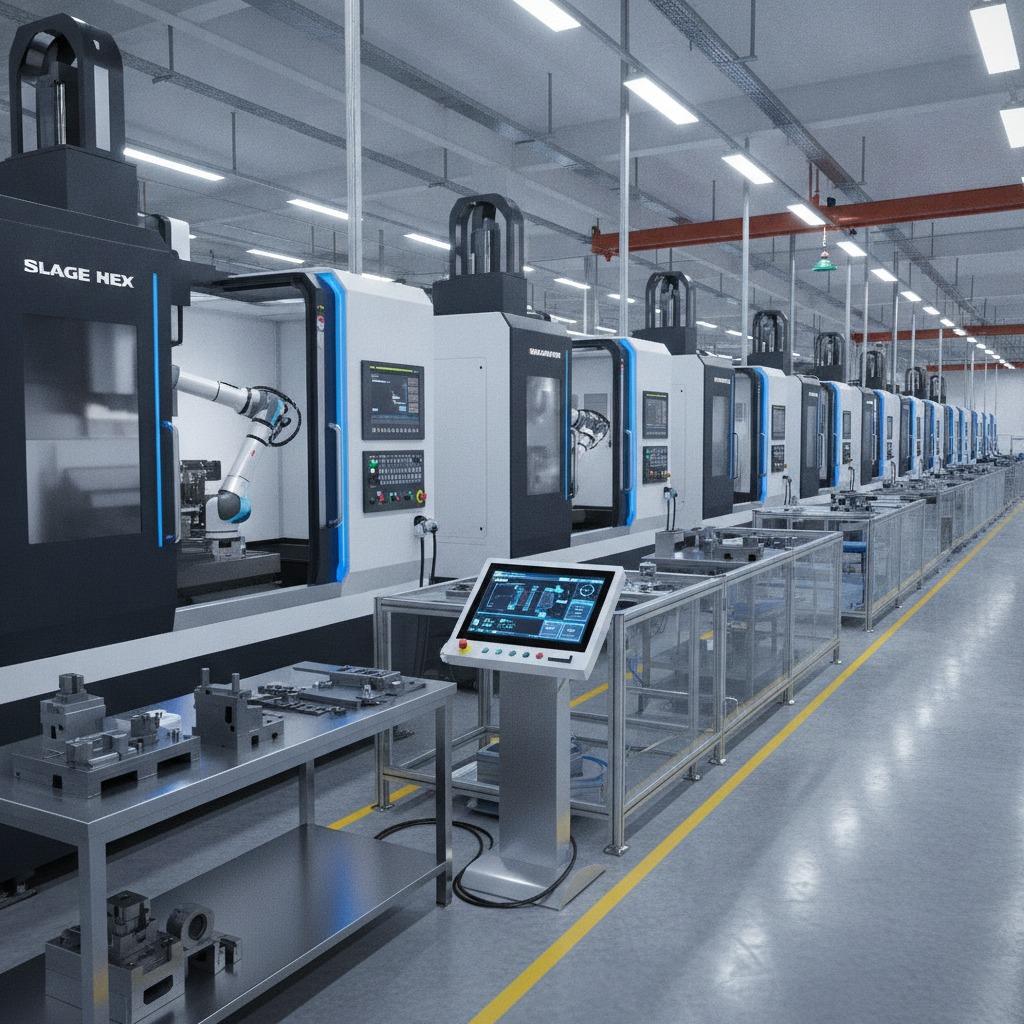
Datum Contract First: Working Map
| Contract item | Acceptance question | Record |
|---|---|---|
| Base | Is the plate supported and flat? | Stock, support and flatness data |
| Grid | Are holes and slots related correctly? | Datum, coordinates and raw results |
| Threads | Can fasteners seat and repeat? | Pitch, depth, gauge and burr check |
| Clamps | Can fixtures load without distortion? | Clamp sequence and reload trial |
| Handoff | Can the next team use the plate? | Revision, map, inspection and owner |
Write the Datum Contract
Name primary, secondary and tertiary datums, flatness, parallelism, hole position, thread requirements, edge conditions and inspection method. State which features are functional interfaces and which are convenience features. This contract keeps downstream fixture assumptions connected to the plate evidence.
Mark any customer-supplied reference or tolerance interpretation. A plate can be dimensionally complete yet still create ambiguity if the datum used for inspection differs from the datum used for loading. Zhihe CNC recommends resolving that before programming.
Control Stock and Support
Record material, thickness, saw condition, stress relief where relevant, support points, clamping, thermal context and cleaning. Thin or large plates can move when stock is removed or clamps change. The starting state belongs in the acceptance file.
Perform a seating and release observation before final measurement. If the plate changes after unclamping, separate support and process effects from machine or gauge effects. Keep the marked raw data.
Plan the Hole Grid
Group holes by diameter, depth, thread, counterbore, pitch and function. Define datum, probing, tool path, tool life, coolant, burr control and gauge. A CNC machining center for fixture plates creates value when the grid can be reproduced and inspected, not merely when the drilling cycle is short.
Use a coordinate map with hole identity. Keep accepted, held and reworked locations traceable. This matters when a downstream fixture references one hole family and a later revision changes another.
Protect Threads and Seating Faces
Separate drilling, tapping, counterboring and surface finishing evidence. Record tap type, pitch, depth, entry, lubrication, chips and gauge. Protect seating faces from burrs and scratches during handling, cleaning and inspection.
Run a controlled tool-life event on a representative thread family. Confirm the replacement, preset, offset and gauge route. Do not release a plate on visual thread appearance alone.
Make Clamping Repeatable
Document clamp locations, force or sequence, support, loading orientation and access for the fixture that will use the plate. Trial unload and reload. The plate should remain identifiable while the fixture is being prepared.
If clamps distort a face or block probing, record the limitation and correct the interface. A datum contract is useful only when the downstream team can honor it.
Probe Before You Cut
Define probing points, warm-up, coordinate transform, datum confirmation and program checksum. Record the probe state and what happens when a check fails. Probing should confirm the contract rather than silently changing it.
Keep a backup of approved programs, offsets and maps. Zhihe CNC recommends a visible revision label on the plate and in the digital file so a shop does not mix two grids.
Inspect the Interface, Not Just the Plate
Measure flatness, parallelism, hole position, thread, counterbore, burr, surface and datum relationship. Include the fixture or gauge interface where practical. A plate that passes isolated dimensions may still fail when a pin, clamp or part is loaded.
Record raw data and disposition by feature. If external inspection is required, include handling, timing, queue and release authority. This prevents the plate from waiting indefinitely for an unowned decision.
Run the Reload Trial
Load the intended fixture or a controlled surrogate, clamp, probe and inspect the key interface features. Record seating, access, chips, cleaning, operator steps and repeatability. The trial turns a drawing contract into an operating check.
Repeat after cleaning or a planned tool event where practical. Note any manual correction. A CNC machining center for fixture plates should support the next operation without undocumented interpretation.
Cost the Support Route
Count setup, tooling, probing, cleaning, deburring, inspection, held work, maintenance and documentation against released plates. Do not compare only cutting time. Fixture plates often carry high value in their interface quality and traceability.
State batch size, revision frequency, material, gauge access and staffing. Zhihe CNC uses the support ledger to show where a design or fixture change would have the greatest effect.
Freeze the Handoff Package
Include drawing revision, datum map, hole chart, thread results, surface data, programs, offsets, fixture notes, inspection file, cleaning rule, storage and owner. Keep superseded versions accessible but clearly marked.
At handoff, review the open list with engineering, quality, production and maintenance. Keep the effective revision, document location and approval authority visible.
Evidence Ledger
| Interface risk | Typical symptom | Evidence to repeat |
|---|---|---|
| Datum shift | Part does not reload to expected relation | Support, probing, clamp and raw position data |
| Thread issue | Fastener binds or lacks depth | Tap, chips, gauge, tool life and cleaning |
| Face distortion | Flatness changes after release | Support, clamp sequence and release measurement |
| Grid error | Fixture pins do not align | Coordinate map, datum and inspection route |
Make the Plate a Controlled Interface
A fixture plate continues to create value after machining only when its map, revision, inspection and storage remain controlled. Mark the physical plate, protect reference faces and make the digital file easy to find. If a hole is repaired, plugged or reworked, record the change before the plate returns to service.
Review the interface with the next fixture owner, not only with the machine operator. The reload trial and datum contract should be understandable to production, quality and maintenance. Zhihe CNC recommends a named owner for the plate baseline so a later design change does not quietly invalidate the grid.
Audit the First Fixture That Uses the Plate
A fixture plate machining center acceptance is stronger when the first downstream fixture is included in the review. Check pin seating, clamp access, datum repeatability, chip clearance and the time required to confirm the grid. This does not replace plate inspection; it demonstrates that the interface can be used as intended. Zhihe CNC records any manual shim, cleaning step or correction as part of the operating baseline.
If the fixture plate machining center route changes material, thickness, grid, tool interface or inspection equipment, reopen only the affected clauses but preserve the previous release file. That keeps change control proportional and avoids repeating every operation unnecessarily. Name the effective revision, document location and approval authority before the plate returns to production.
Protect the Interface After Delivery
The fixture plate machining center file should remain with the physical plate, fixture map and inspection record. A fixture plate machining center creates repeatability only when the grid, datum and revision can be found by the people who load the next job.
Review the fixture plate machining center baseline after a repair, plugged hole, new clamp or changed gauge. Repeat the affected evidence and mark the effective revision. This keeps a useful interface from becoming an undocumented exception on the shop floor.
Buyer FAQ: fixture plate machining center
What is a datum contract?
A shared definition of reference surfaces, relationships, tolerances, inspection and downstream use.
Why is support important for fixture plates?
Stock removal and clamping can change flatness or datum relationships.
How should a hole grid be documented?
Use hole identity, coordinates, diameter, depth, thread, datum, tool and raw inspection result.
Should drilling and tapping be released together?
No. Separate hole geometry, thread depth, entry, chips, gauge and tool-life evidence.
What is a reload trial?
A controlled load, clamp, probe and inspection check using the intended fixture interface.
How does Zhihe CNC handle revisions?
Zhihe CNC preserves the old baseline, labels the effective revision and repeats affected evidence.
What belongs in the handoff package?
Drawing, datum map, hole chart, programs, offsets, fixture notes, inspection, cleaning and ownership.
Can visual inspection release a thread?
No. Use the declared gauge, depth, entry, burr and sampling route.
What should capacity include?
Setup, tools, probing, cleaning, deburring, inspection, holds, maintenance and documents.
What should buyers send?
Send plate drawings, material, datum, grid, threads, fixture interface, volume and inspection requirements.
Bring the Decision to Zhihe CNC
Send Zhihe CNC the controlled drawings or CAD, material and stock, critical features, annual volume, batch mix, fixture concept, tool limits, inspection route, site conditions and service region. Review the Zhihe CNC product portfolio, the company and factory profile, and the engineering inquiry route. For fixture plate machining center, request a dated configuration, representative trial, acceptance boundary, open-assumption list and named support owner.
Reference Boundary
The ISO machining-centre reference and OSHA machine-guarding guidance offer machine-test or safeguarding context. They do not replace drawing-specific acceptance, local risk assessment, product certification, regulatory release or the buyer's operating procedures.





