

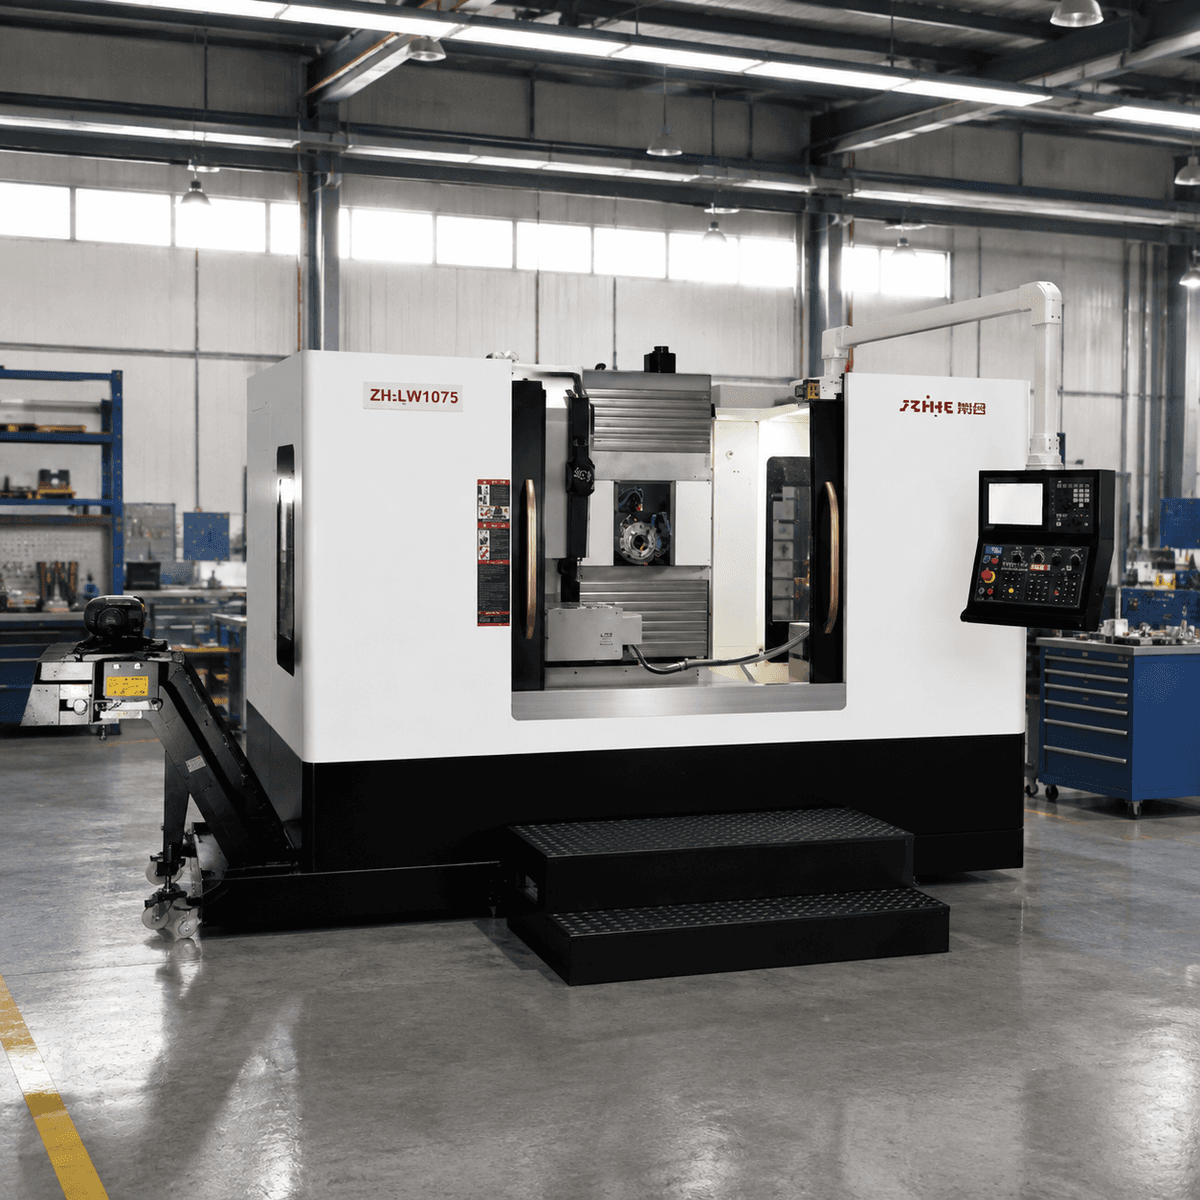
CNC machining center tool capacity should be planned from the tool assemblies a production schedule needs, not from the number of cutters on the purchasing list. A cutter may need a second holder for a different reach. A frequently used tool may need a replacement ready in the magazine. Another tool may belong to a different material group and should not be treated as interchangeable.
For a high-mix shop comparing Zhihe CNC configurations, the important question is therefore not simply “How many pockets are available?” It is “Which jobs can stay ready without disrupting the next job?” The method below turns that question into a tool list, a calculation and a purchasing decision.
Start with three real jobs, not the biggest number
Select a routine job, a tool-intensive job and a job that changes the material or workholding arrangement. Include the parts that actually compete for the same machine. A list covering every component the company has ever made can produce an oversized requirement that the weekly schedule never uses.
Record each complete tool assembly. Give it an identifier that includes the cutter, holder, relevant reach and intended operation. Two tools with the same cutting diameter do not necessarily perform the same job. The distinction matters when one must reach past a fixture or meet a different surface requirement.
Next, mark which assemblies can genuinely be shared. Have the process owner confirm those decisions rather than assuming that similar names mean interchangeable tools. This is where a CNC machining center tool capacity review often becomes useful: it reveals process assumptions that a pocket count cannot show.
Calculate CNC machining center tool capacity for two jobs
Consider a hypothetical schedule containing Job A and Job B. Job A uses 12 unique assemblies. Job B uses 10. The engineering review confirms that six assemblies are identical and may remain loaded for both jobs.
The combined cutting-tool requirement is 12 + 10 − 6 = 16 assemblies. Suppose the buyer also plans four duplicate assemblies for selected high-use tools and one spindle probe stored in the magazine. The planning total becomes 21 occupied positions before examining any arrangement-specific restrictions.
Now suppose the proposed configuration and tool arrangement require three additional positions to remain unavailable. The planning requirement becomes 24 positions. This final condition is an example assumption, not a statement about a Zhihe model or a universal rule for large tools. Ask the supplier to verify the actual storage and exchange arrangement.
| Illustrative planning item | Positions in this example | Why it is counted |
|---|---|---|
| Job A assemblies | 12 | Complete tools needed for the first job |
| Additional Job B assemblies | 4 | Ten assemblies minus six confirmed shared tools |
| Ready duplicate assemblies | 4 | Buyer-selected replacement provision |
| Stored spindle probe | 1 | Assumed magazine-based probe arrangement |
| Unavailable positions | 3 | Hypothetical configuration and clearance restriction |
| Total planning requirement | 24 | Requirement to validate against an actual machine |
Notice what the total does not contain: a promise that a 24-position magazine would be the right purchase. It would leave no spare capacity under these assumptions. Nor does the example prove that more positions would solve every interruption. Tool condition, identification, measurement and program preparation still matter.
Convert the arithmetic into a specification request
Ask for the constraints that apply to the quoted machine and tool changer. Avoid importing values from another manufacturer's machine, even when both machines use a familiar spindle taper.
| Specification to confirm | Information to send | Question for the quotation |
|---|---|---|
| Nominal and usable positions | Current tool-assembly list | Which positions can be used with this exact arrangement? |
| Tool dimensions and mass | Drawings or supplier data for complete assemblies | What storage, exchange and spindle limits apply? |
| Tool identification | Proposed tool numbers and job families | How are tools and assigned positions managed? |
| Measurement and replacement | Presetting and tool-checking workflow | Which functions and hardware are included? |
| Material groups | Workpiece materials, tools and coolant constraints | Which assemblies can remain shared across the schedule? |
| Future growth | Known next jobs, not an arbitrary percentage | What upgrade paths are technically available? |
Haas publishes machine-specific operating information through its official manual library. That is a useful example of why the correct machine documentation matters. It is not a source of capacity specifications for Zhihe CNC. For the machine being purchased, request the corresponding approved specifications and instructions.
A larger magazine is one option, not the whole plan
Four approaches can address a shortage. Their usefulness depends on where the interruption actually occurs.
| Configuration or workflow | When it may suit the shop | Question to resolve before buying |
|---|---|---|
| Existing magazine with planned tool changes | Small batches with predictable operator attendance | Can tool preparation happen before the machine stops? |
| Larger magazine option | Many confirmed assemblies must remain ready | Are dimensions, mass and exchange restrictions acceptable? |
| Smaller common tool set | Several jobs can use genuinely compatible assemblies | Does the shared tool compromise the operation or surface? |
| External preparation plus orderly changeovers | Tools are available but searching and setting consume time | Are identifiers, measurements and job kits reliable? |
For CNC machining center tool capacity, the cheapest nominal solution may create repeated manual preparation. The largest nominal solution may carry assemblies that the shop rarely uses. Compare each option against the same schedule and tool list so the discussion stays grounded.
Keep measurement separate from storage
A loaded tool is not necessarily ready to cut. The process still needs correct identification, relevant offsets and an agreed method of checking condition. A storage plan that ignores these steps can make the machine look prepared while leaving the operator to resolve the uncertainty.
Renishaw's machine-tool probing and measurement overview describes tool measurement and workpiece measurement as distinct applications. For a buyer, the practical question is where each required check takes place and what information it supplies. Do not assume that purchasing a probe automatically defines the entire workflow.
Include the people who prepare tools in the comparison. Ask them to follow one assembly from the toolroom to the machine, through a replacement, and back to storage. Missing labels, unclear ownership and inconsistent job sheets are purchasing information, not merely operator inconvenience.
What materials and duplicate tools change
Material changes can alter the required cutter, geometry or operating approach. Review those choices with the tooling and process specialists. A pocket saved by sharing an unsuitable assembly is not a useful saving. Conversely, creating separate assemblies for every job without checking commonality can inflate the requirement unnecessarily.
Duplicate tools also need a reason. Name the operation they protect and the expected production period. Ask how replacement is selected, how the correct offset is associated with it and what stops the process if the replacement is not ready. Specify the needed function rather than assuming it is standard on every controller.
These are configuration and process questions. They are not instructions to alter tool-changer parameters or bypass machine limits. Loading, recovery and maintenance must follow the delivered machine documentation and be performed by appropriately trained personnel.
Take the plan into the Zhihe CNC quotation
Zhihe CNC's company profile describes custom machine solutions and project-based production scheduling. Use the tool-assembly list to ask which available configuration fits the intended work. Request any magazine option, measurement equipment, controller functions and training as identifiable quotation items.
Ask about delivery impact before treating an option as a simple accessory. Also separate the machine price from holders, presetting equipment, tooling, installation and training. If a supplier proposes a different configuration, compare it with the same tool list and production assumptions.
For quality documentation, specify the inspection or demonstration you need. Ask for a trial that uses representative assemblies, including the difficult one, within the approved limits. Request relevant certificates separately where required; a successful tool-change demonstration is not proof of an unrelated certification.
Ten decisions that tend to come up in review
Should nominal pocket count equal the calculated requirement?
Not automatically. Examine usable positions, the actual assembly arrangement and known future jobs. A calculation that uses every position under ideal assumptions may be too fragile for the intended schedule.
Can two jobs share a tool with the same diameter?
Only after confirming the full assembly and process requirements. Reach, holder, cutting geometry, material and required condition may differ even when the nominal diameter matches.
Must every tool have a duplicate?
No. Choose duplicates around the operations and production periods that justify them. Record the reasoning so the requirement does not become an unexplained blanket allowance.
Does a spindle probe always occupy a magazine position?
The answer depends on the installed arrangement. Count the actual storage method specified for the proposed machine; the calculation above explicitly assumes a magazine-stored probe.
Is maximum tool length enough information?
No. Ask about the complete storage, exchange and working arrangement, including applicable mass and dimensional limits. The actual assembly and fixture need to fit the approved configuration.
Is a tool magazine upgrade always possible later?
Do not assume so. Obtain a configuration-specific answer covering mechanics, controls, installation, downtime and support. A future option should not be treated as available until confirmed.
How should a shop estimate future CNC machining center tool capacity?
Use known part families and plausible schedules. Keep speculative work separate. This makes the reason for added capacity visible without pretending that every possible future job is certain.
Will more CNC machining center tool capacity reduce setup time?
It can address repeated loading of required assemblies, but it does not fix missing job information or unprepared tools. Measure the actual delay before choosing the improvement.
What belongs in a tool-capacity trial?
Use the agreed tool list, representative jobs and relevant replacement events. Verify identification and preparation as well as physical storage. Follow the supplier's approved operating and safety procedures.
What should I send with an inquiry?
Send the job families, complete assembly list, shared-tool decisions, material groups and required production period. Include the difficult assembly drawings and any intended probing or replacement functions.
Put the uncertain positions on paper
Before requesting a bigger machine, circle every position in the CNC machining center tool capacity calculation that rests on an assumption. Those circles are the most useful questions for an engineering discussion.
Use Zhihe CNC's inquiry page to request a proposal against that list. A clear answer about usable capacity, included functions and preparation responsibilities is worth more than a pocket count considered in isolation.





